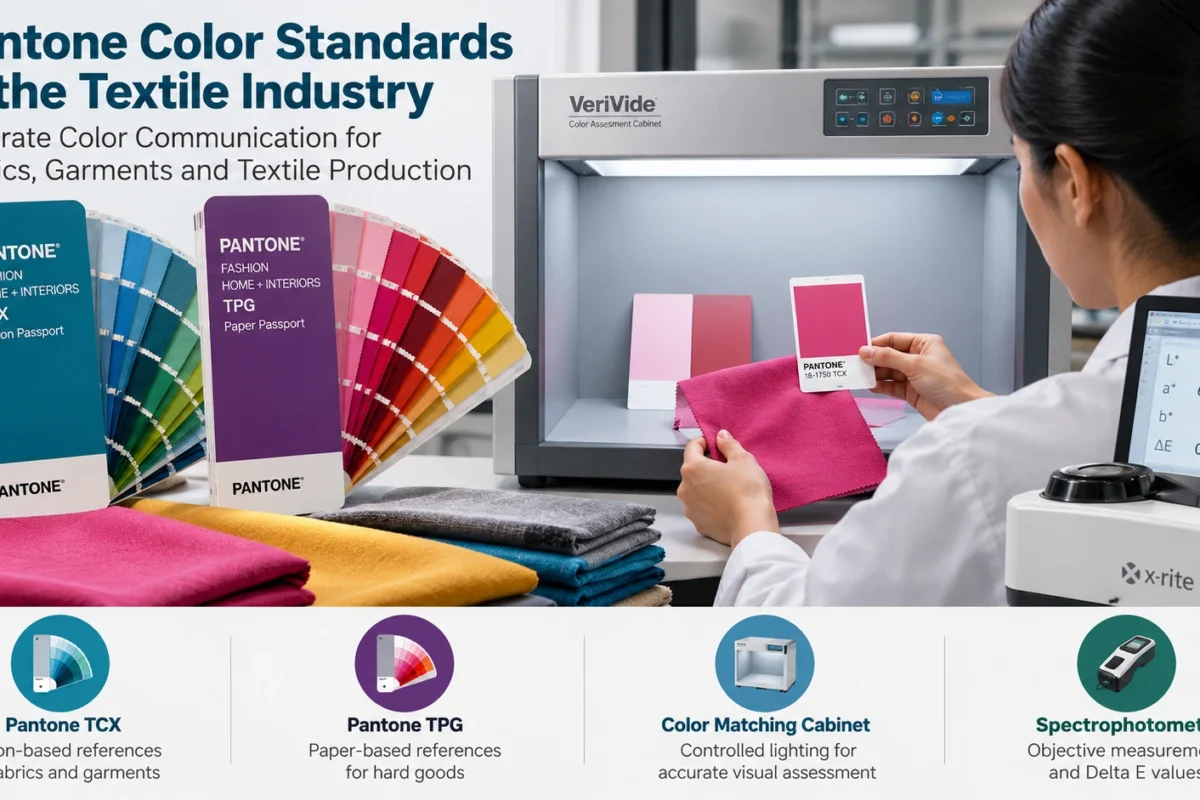
Pantone Color Standards references arranged beside fabric swatches for textile color matching

Pantone Color Standards for Textile Industry: Complete Guide

Pantone Color Standards give textile teams a shared language for color. When a designer, a dyeing unit, a garment factory and an overseas buyer must agree on one shade, a numbered physical reference removes a lot of guesswork. That matters in fabric development, dyeing, garment manufacturing and export quality control. It does not remove variation by itself, so this guide also covers how to use it well.

What Are Pantone Color Standards?

Pantone Color Standards are numbered, named color references that let people specify a target shade without describing it in words. A designer picks a code, the supplier receives the same code, and both compare their work with a physical reference. For textiles, the relevant system is Pantone Fashion, Home + Interiors (FHI).

A reference communicates a target. It does not guarantee an identical match on every fiber, finish or light source.

What are Pantone Color Standards?
Pantone Color Standards are numbered, named color references used to specify and communicate target shades across design, production and approval. In textiles, they give designers, mills, dyeing units and buyers a shared point of comparison, although the match on fabric still depends on material, finish and lighting.

Why Are Pantone Color Standards Important in the Textile Industry?

A shared reference matters most where several parties handle the same color:

  • Specification: one code replaces vague descriptions like “dark navy”.
  • Fabric and yarn development: teams know which shade they are aiming for.
  • Dyeing and finishing: recipes can be built and corrected against a known target.
  • Lab dip approval: buyer and supplier judge submissions against the same reference.
  • Bulk production: the approved standard gives production something to check against.
  • International trade: a code travels across borders more reliably than a verbal description.

This reduces avoidable discrepancies, but it cannot eliminate them. Fiber, dye chemistry and finishing still shape the result.

Why are Pantone Color Standards important in textiles?
They give buyers, mills and garment makers a common reference for specifying, developing and approving colors. This reduces miscommunication during lab dips and bulk production, especially in international sourcing, although fabric composition, dyeing and lighting still influence the final appearance.

Different Types of Pantone Color Guides Used in Textiles

Pantone offers several reference systems, and they are not interchangeable. Within Pantone Fashion, Home + Interiors, TCX references show colors on cotton, while TPG references show the same system as a lacquer on coated paper. Pantone positions TPG for hard goods such as ceramics, paint, cosmetics, accessories and leather, and TPG colors are designed to match back to TCX. The Pantone Formula Guide is a print and graphic design system, so don’t treat it as a textile reference by default.

Pantone Reference General Application Important Consideration
Fashion, Home + Interiors (FHI) Fashion, textiles, interiors Parent system; confirm which format the buyer specifies
TCX (cotton) Fabrics, garments, soft goods Cotton-based, so closest to a textile substrate
TPG (paper) Hard goods, accessories, leather Lacquered paper; matches back to TCX but is a different surface
Formula Guide Graphic design and print Ink on paper; not textile-specific

Always confirm the exact guide, edition and format with your buyer, and check Pantone’s official site for current product names.

What is the difference between TCX and TPG?
TCX references show Pantone FHI colors on cotton, suited to soft goods like fabric and garments. TPG references show the same system on lacquered coated paper, suited to hard goods such as accessories and leather. TPG colors are designed to match back to TCX, but they are different surfaces.

How Pantone Color Standards Work in Fabric Color Matching

A typical workflow looks like this:

  1. Select the reference the buyer specifies.
  2. Send the exact color code to the supplier.
  3. Prepare a lab dip or fabric sample.
  4. Compare the sample against the agreed reference.
  5. Assess it under suitable lighting.
  6. Measure color difference instrumentally when required.
  7. Obtain buyer approval before bulk production.
  8. Run production checks to monitor consistency.

A good lab dip can still look “off” because the standard and your fabric are different materials. Fiber composition, dye chemistry, construction, texture and finishing all change how light reflects, so one color can look different on cotton, polyester or a brushed surface.

How do textile manufacturers match fabric colors to Pantone references?
They receive the specified code, prepare lab dips, and compare them with the physical reference under controlled lighting. Where required, they measure color difference with a spectrophotometer, then seek buyer approval before bulk dyeing and keep checking production batches.

Pantone Color Standards vs. Digital Color Codes

RGB and HEX describe color as light mixed on a screen. A Pantone reference is a physical object seen by reflected light. The same HEX code can look different on two devices, and neither reproduces a dyed fabric exactly.

Aspect Pantone physical reference RGB / HEX
Medium Physical sample Light emitted by a screen
Viewing Reflected light; depends on the light source Depends on device, brightness, calibration
Best use Specification and approval Early design and quick sharing
Limitation Specific to its substrate Cannot represent every textile color

Use screens for early concepts and physical references for approval.

Can a Pantone color look different on fabric and on a screen?
Yes. Screens emit light and vary by brightness and calibration, while fabric reflects light and is affected by fiber, texture and finish. A digital swatch is only an approximation, so approvals should rely on physical references and samples.

The Role of a Color Matching Cabinet and Light Booth

A color matching cabinet, often called a light booth, gives evaluators a controlled environment for visual assessment. Instead of judging a shade near a window or under factory tube lights, they compare the approved reference and the production sample under defined light sources with neutral surroundings.

This matters because of metamerism: two samples can match under one light and differ under another, often because different dyes or pigments were used. Checking under more than one light source exposes this before bulk goes out.

Which illuminants and procedure apply depends on the buyer’s requirements and the relevant test protocol, so follow the buyer’s instruction rather than assuming a default.

Why is a color matching cabinet used in textile quality control?
It provides standardized, repeatable lighting so evaluators can compare fabric samples with approved references fairly. It also helps reveal metamerism, where colors match under one light source but differ under another, before bulk production proceeds.

How Spectrophotometers and Delta E Help with Color Assessment

A spectrophotometer measures the light a fabric reflects across the visible spectrum and converts it into numerical color data. Delta E (ΔE) expresses the difference between two measured colors, such as standard versus sample, as a single number.

What a given ΔE means depends on the color-difference formula, measurement conditions, the material and the buyer’s acceptance criteria. There is no universal limit that suits every fabric or customer, so use the tolerance in the buyer’s specification. Instrument data complements visual assessment rather than replacing it. Numbers are objective and repeatable, while visual checks catch what the end customer will actually see.

Common Challenges in Pantone Color Matching

Typical causes of color variation include:

  • Fiber composition, dye selection and dye concentration
  • Fabric construction and surface texture
  • Dyeing and finishing conditions, and batch-to-batch variation
  • Different lighting, and different instrument settings or measurement conditions
  • Comparing a physical reference with a screen
  • Choosing the wrong reference, such as a print-oriented guide for fabric
  • Weak lab dip approval procedures

Practical fixes: confirm the reference system in writing, fix the lighting and measurement conditions, and agree how many lab dip rounds and which criteria apply.

How to Maintain Color Consistency in Textile Production

  • Use the agreed reference and record the color code, edition and approved sample details.
  • Prepare and evaluate samples the same way every time.
  • Assess under agreed lighting, and add instrumental readings when specified.
  • Document buyer-approved acceptance criteria and every lab dip approval.
  • Monitor bulk dyeing and finishing batches against the approved standard.
  • Report deviations to the buyer before production continues.

A Pantone reference says what the color should be, not how well it will hold up. Rubbing and wash fastness are tested separately with crock meters and wash-fastness testing instruments.

Choosing the Right Pantone Color Products for Your Business

Start with the application. A mill working to a buyer’s TCX specification needs a cotton-based guide, while a team developing accessories may need TPG. Don’t substitute a print-oriented Formula Guide for textile work. Then consider how many colors you need, whether you need physical guides for every desk, how updates and replacements are handled, and whether the guide matches what your buyers specify. Finally, decide whether you also need a color matching cabinet or other testing equipment to evaluate samples consistently.

Pantone Color Standards in India’s Textile and Garment Industry

India’s textile industry spans fabric dyeing and processing through to garment manufacturing. Business and sourcing hubs such as Bangalore and Tiruppur show how many parties may handle one color before it reaches a retailer: textile exporters, processing units, buying house teams and international buyers. When each reads the same code from the same physical reference, fewer shade questions travel back and forth across time zones. Buyer requirements commonly name the reference system and approval steps, so confirm them at the start of an order.

Why Choose Amith Garment Services?

Amith Garment Services is a Bangalore-based supplier of textile testing and quality-control instruments, established in 1999 according to its website. Its range includes Pantone color standards, fabric inspection machines, GSM cutters, crock meters, bursting strength testers and colour fastness testing instruments, along with calibration services. Labs that check color usually also check GSM, rubbing fastness, fabric defects and strength, so planning instruments as one workflow can simplify setup. Explore the Pantone Color Standards page, or contact the team through the website for product information.

Conclusion

Pantone Color Standards help teams communicate target colors and stay coordinated from development to delivery. They work best alongside suitable lighting, documented lab dip approvals and consistent quality-control checks, with instrumental measurement added when the buyer requires it. Put those pieces in place, and your team will get far more from Pantone Color Standards.

Frequently Asked Questions:

1. What are Pantone Color Standards in the textile industry?

Pantone Color Standards are numbered, named color references that help designers, mills, dyeing units, garment manufacturers and buyers agree on a target shade. In textiles, the relevant system is Pantone Fashion, Home + Interiors, which includes cotton-based TCX and paper-based TPG references. A reference communicates the intended color, but the final result on fabric still depends on fiber, dyes, finishing and the lighting used for assessment.

2. What is the difference between Pantone TCX and TPG?

TCX references present Pantone Fashion, Home + Interiors colors on cotton, making them suitable for fabrics, garments and other soft goods. TPG references present the colors on coated paper with a lacquer finish and are intended for hard goods such as ceramics, paint, cosmetics, accessories and leather. TPG colors are designed to match back to TCX, but the surfaces differ, so confirm which format your buyer specifies.

3. How do Pantone references help with fabric color matching?

Pantone references give everyone the same color target. The buyer specifies a code, the supplier prepares a lab dip or sample, and the team compares it with the physical reference under agreed lighting. Where required, a spectrophotometer provides Delta E color-difference measurements. Buyer approval should be obtained before bulk production. The reference supports communication and comparison but cannot guarantee an exact match on its own because fabric and finishing influence color.

4. Which equipment helps assess textile colors accurately?

Visual assessment is usually performed in a color matching cabinet or light booth, which provides controlled lighting for comparing samples with approved references. A spectrophotometer adds objective measurements and Delta E values. Physical Pantone guides provide the color reference, while lab dyeing equipment supports lab dip preparation. The appropriate illuminants, formulas and tolerances depend on buyer requirements and the relevant test protocol.

5. What are Pantone Color Standards used for?

Pantone Color Standards are used to select, describe and approve specific colors. In textiles, they help designers, mills and buyers agree on a shade so everyone works toward the same target during product development and production.

6. How do I match a fabric to a Pantone color?

Start with the Pantone code specified by the buyer. Prepare a lab dip, compare it with the physical reference under controlled lighting, and measure the color difference if required. Obtain buyer approval before starting bulk production.

7. What is the difference between TCX and TPG?

TCX presents Pantone Fashion, Home + Interiors colors on cotton, making it suitable for fabric and garment applications. TPG presents the colors on coated paper and is intended for hard goods such as accessories. Confirm which format the buyer requires before ordering.

8. Which equipment helps check fabric color under standard lighting?

A color matching cabinet, also called a light booth, provides controlled lighting for comparing fabric with a color reference. A spectrophotometer can provide measured color-difference data when required by the buyer or testing procedure.
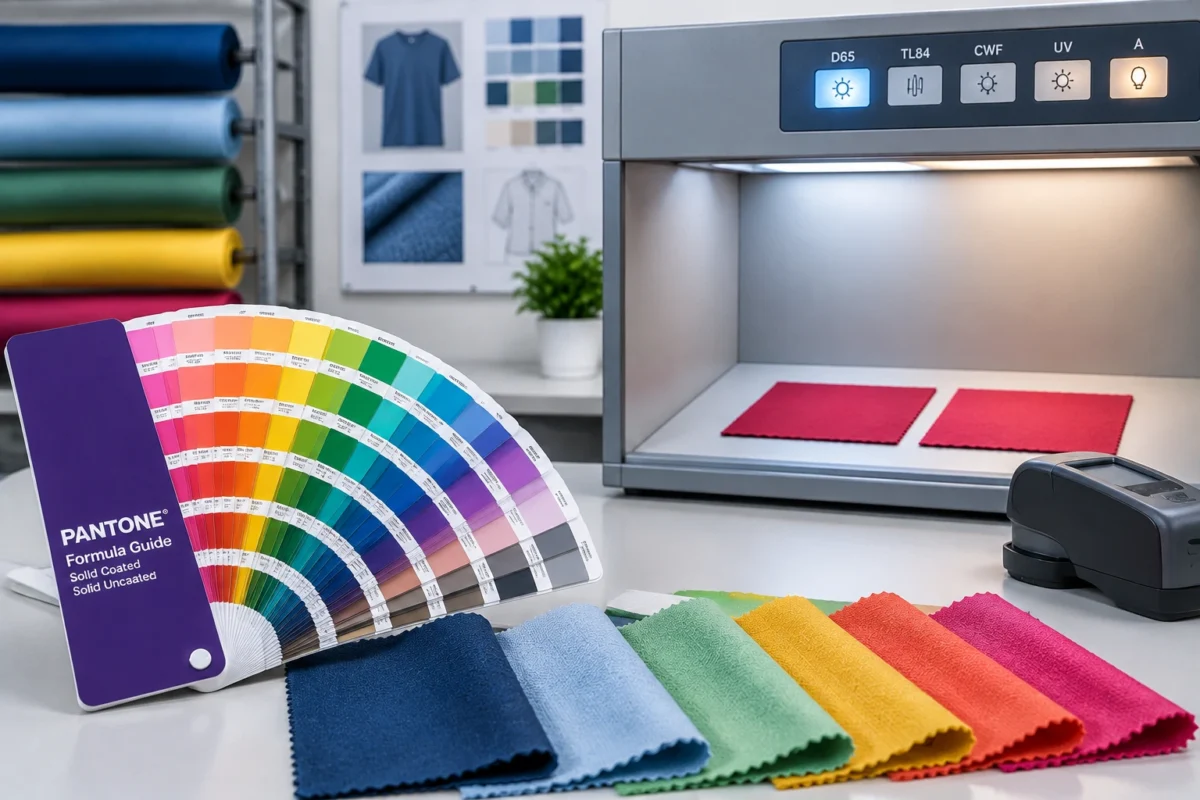
Pantone Color Standards used for textile colour matching and quality control

What Are Pantone Color Standards and Why Are They Important?

What Are Pantone Color Standards?

Pantone Color Standards are the standardized colour references built around the Pantone Color System, where each shade carries its own identifier. A name like “sky blue” is open to interpretation. A code is not.

For textiles, designers typically cite codes from Pantone’s fashion and home range, often supplied as cotton-based swatches (TCX). Manufacturers then treat that code as the target during development, lab dipping and production.

Pantone Color Standards are standardized, coded colour references that let designers, buyers and manufacturers specify the same shade without relying on subjective names. Each colour has a unique identifier, which reduces misunderstandings during development, sampling and production, especially across suppliers and countries.

Why Are Pantone Color Standards Important in Textile Manufacturing?

Colour is usually the first thing a buyer notices and the first reason a shipment is questioned. A shared reference helps at every stage: fabric development, sampling, dyeing, printing, bulk production, buyer approvals and export documentation.

Picture a knitwear order. The buyer sends a code, the mill dyes a lab dip, and the garment factory cuts panels from two dye lots. Without a common reference, each party judges “close enough” differently. With one, the disagreement becomes a discussion about measurable deviation rather than opinion.

Why are they important? They give everyone in the supply chain the same colour target. That reduces sampling rounds, limits shade disputes, supports buyer approvals and makes quality control more objective across fabric, printing and garment production.

How Do Pantone Color Standards Work?

The usual workflow looks like this:

  1. The buyer or designer selects a colour reference.
  2. The code is communicated to the manufacturer.
  3. Lab dips or fabric samples are prepared.
  4. Colour is evaluated under controlled lighting.
  5. Recipes are adjusted where necessary.
  6. The approved shade becomes the production reference.
  7. Bulk production is checked against that approved standard.

How are Pantone colours used in textiles? Designers cite a code in the tech pack, mills and dyeing units use it as the lab-dip target, and quality teams compare bulk fabric or garments against the approved shade under controlled light.

One caution: the same code will not look identical on every material. Fibre type, dye chemistry, fabric construction, finishing, surface texture, printing method and viewing conditions all shift appearance. A Pantone reference is a target, not a guarantee of an exact physical match on every substrate.

Pantone Color Standards vs Pantone Colour Guides

The two terms are often used interchangeably, but they play different roles. Broadly, the standards are the coded colour references. The guides are the tools that present them.

Factor Pantone Color Standards Pantone Colour Guides
Purpose Define and codify reference colours Present those colours as physical or digital swatches
Colour Reference The coded shade identity A printed or dyed representation of it
Manufacturing Use Target for development and approval Visual aid in the office, lab or floor
Textile Application Specifying fabrics, trims and garments Substrate-specific guides (e.g., cotton) for selection
Quality Control Basis for deviation checks Visual comparison only; sensitive to light and ageing
Buyer Communication Codes in tech packs and approvals Shows intent alongside the code

Pantone offers several systems and formats, and the Pantone Matching System (PMS) is best known in print. Always confirm which one your buyer specifies.

Why Is Pantone Colour Matching Important for Fabrics?

Pantone colour matching links design intent to real cloth. It shapes shade development, lab dips, dyeing, fabric inspection, buyer approval and shade consistency in bulk.

What is Pantone colour matching? It is the process of adjusting a dye or print recipe until a fabric sample aligns with a chosen Pantone reference within an agreed tolerance, usually checked under standardized lighting before buyer approval.

Ordinary office light or window daylight is a poor judge. Both change through the day and with the weather. Controlled lighting gives every evaluator the same conditions, so a disagreement reflects the fabric, not the room.

Role of a Color Matching Cabinet in Pantone Colour Evaluation

A Color Matching Cabinet, also called a light booth, provides standardized light sources inside a neutral enclosure. Common options include daylight simulation, TL84 store lighting, and incandescent or UV sources.

Why several? Metamerism. Two samples can match under one illuminant and visibly differ under another, often because different dyes were used. Checking under multiple sources exposes this before the buyer does. This textile laboratory equipment lets mills, factories and buyers compare shades under the same conditions.

What is the difference between Pantone and a colour matching cabinet? Pantone supplies the colour reference; the cabinet supplies the lighting to judge it. One defines the target, the other standardizes how you view the target and the sample.

Why is controlled lighting important? Colour appearance changes with the light source. Standardized illuminants and neutral surroundings let evaluators compare shades consistently and reveal metamerism, so decisions don’t depend on time of day, weather or room.

Pantone Color Standards and Textile Quality Control

Standardized references support quality control at each checkpoint:

  • Incoming fabric inspection: confirming supplied fabric against the reference
  • Lab dip approval: documenting the accepted shade
  • Production monitoring: catching drift between dye lots
  • Shade grouping: keeping panels from the same garment visually consistent
  • Final inspection and buyer approval: verifying against the signed-off standard

Colour consistency shapes perceived quality. A sleeve slightly off from the body panel reads as a defect, even when every strength test passes.

Factors That Can Affect Colour Matching

  • Fibre and construction: the same dye looks different on cotton, polyester or a textured knit.
  • Dye selection and concentration: small recipe changes shift the shade.
  • pH, temperature and processing time: a bath that runs slightly hotter or longer can change results.
  • Finishing: softeners and resin finishes may alter depth or tone.
  • Viewing conditions: lighting, viewing angle and surface gloss change perception.
  • Instrument calibration and sample preparation: uncalibrated devices or unevenly conditioned samples give misleading comparisons.

Pantone Color Standards in Garment Exporting

International buyers often specify colours by code, and Indian manufacturers, dyeing houses and fabric suppliers work from the same reference. In hubs such as Tiruppur, where knitwear exporters manage large repeat orders, and in Bangalore’s garment manufacturing sector, that shared reference helps keep shade expectations aligned across the textile industry. For textile exporters, a documented approved standard also makes it easier to resolve questions after shipment.

How to Maintain Better Colour Consistency in Textile Production

  • Use a defined colour reference for every order.
  • Keep approved lab-dip standards on file.
  • Evaluate shades under controlled lighting.
  • Hold dyeing and finishing parameters steady.
  • Calibrate relevant instruments.
  • Compare bulk production with the approved sample.
  • Record shade deviations and maintain testing documentation.
  • Train quality-control personnel.

Distinguish the two assessment methods. Visual assessment relies on trained observers under standard light. Instrumental measurement uses a spectrophotometer to quantify colour difference numerically. Most laboratories use both, and both are commonly guided by AATCC and ISO practices.

Choosing the Right Textile Colour Testing Equipment

Consider the application, testing requirements, lighting needs, compatibility with the standards your buyers use, and how the equipment fits your laboratory workflow. Then look at repeatability, calibration, ease of operation, maintenance, documentation and production volume. A small sampling unit and a large export facility may need very different textile testing equipment. Garment testing instruments for colour should sit alongside those for fastness and physical properties, not in isolation.

Why Choose Amith Garment Services?

Amith Garment Services provides textile testing equipment and related solutions for textile and garment quality-control applications. The range relevant to colour and fabric evaluation includes the Color Matching Cabinet, Crock Meter, Washing Fastness Tester, GSM Cutter, Fabric Inspection Machine, Bursting Strength Tester and Fabric Rolling Machine. Together, these help laboratories check colour, fastness and physical properties in one workflow. For advice on matching equipment to your testing requirements, contact the team through the website.

Conclusion

Pantone Color Standards turn subjective colour talk into a shared, documented reference that suits the realities of textile manufacturing. They work best when combined with lab dips, controlled lighting, calibrated instruments and disciplined records. Used that way, they help mills, factories and exporters deliver colour their buyers expect.

Frequently Asked Questions

Pantone Color Standards are used to specify, communicate and verify colour throughout textile production. Designers cite a code in the tech pack, mills and dyeing units use it as the target for lab dips, and quality teams compare bulk fabric or finished garments against the approved shade. Because the reference is coded rather than described in words, it cuts down on misinterpretation between buyers, factories and suppliers. It works best when paired with controlled lighting and, where required, instrumental colour measurement.

Pantone colour matching gives garment manufacturers a clear target from the first sample. Merchandisers can brief the dyeing unit with a code instead of a vague description, which can shorten lab-dip rounds and reduce shade disputes at approval. During production, the approved standard lets quality teams judge whether dye lots and panels stay within tolerance. It also supports smoother communication with international buyers, who often specify colours by code, though the final match still depends on the fabric and process.

Not always. A Pantone reference is a colour target, but fabrics respond differently to dyes and finishes. Fibre type, yarn and fabric construction, dye class, finishing and surface texture all influence how a shade appears, so a colour achieved on cotton may look different on polyester or a textured knit. Some colours may also fall outside what a given dye system can reproduce. Manufacturers therefore prepare lab dips, evaluate them under standardized light, and agree tolerances with the buyer rather than assuming an identical match.

A Color Matching Cabinet provides standardized, repeatable lighting so shade comparisons don't depend on the time of day, weather or room. Most offer several light sources, such as daylight, store lighting, and incandescent or UV, which helps reveal metamerism, where samples match under one light but not another. Using the same conditions at the mill, the factory and the buyer's office makes Pantone Color Standards easier to apply consistently. It supports visual assessment but does not replace instrumental measurement when numerical data is required.

They define and communicate colour with a code instead of a description. In textiles, buyers and manufacturers use them to agree on a shade, prepare lab dips, and check bulk production against the approved colour.

First, the buyer picks a Pantone code. The mill prepares lab dips to match it, and the shade is checked under controlled lighting. Once approved, that sample becomes the production standard, and bulk fabric is compared against it.

Because a code means the same thing to everyone. Instead of arguing over what "olive green" means, buyers, dyeing units and garment factories work from one reference, which cuts down on shade misunderstandings and rework.

Place the fabric and the approved standard side by side in a colour matching cabinet, then view them under standard light sources such as daylight. If needed, confirm with a spectrophotometer to measure the colour difference numerically.

Pantone swatch fan deck used for textile color approval

 How to Use Pantone Swatches for Accurate Fabric Color Matching

Anyone who has worked on the production floor of a dyeing unit knows how quickly a color approval can go wrong. A shade that looked perfect under the factory tube light suddenly looks “off” the moment the buyer opens the shipment under daylight. This is one of the most common — and costly — problems in textile manufacturing, and it’s exactly why Pantone Swatches exist.

Pantone swatches give manufacturers, dyers, merchandisers, and buying houses a shared, standardized language for color. Instead of relying on memory or subjective judgment, everyone in the supply chain — from the dye house in Tiruppur to the buying office in Bangalore to the brand headquarters overseas — can refer to the same physical reference point. That shared reference is what makes fabric color matching repeatable, rather than a guessing game.

In this article, we’ll walk through what Pantone swatches actually are, how they fit into the broader color approval workflow, the mistakes that most commonly derail shade matching, and how to choose genuine Pantone color products for your lab or production unit.

What Are Pantone Swatches?

Pantone swatches are physical color reference chips, cards, or fan decks produced under the Pantone Matching System (PMS) — a standardized color identification system used globally across textiles, printing, plastics, and design industries. Each swatch carries a unique code, so a shade referred to as “Pantone 19-4052 TCX” means the exact same color whether it’s being discussed in a mill in India or a design studio in Europe.

For the textile industry specifically, Pantone publishes dedicated fashion and home (FHI) color libraries, including cotton-based TCX chips and paper-based TPG chips, formulated to reflect how colors actually appear on fabric rather than on printed paper or plastic.

A few practical points worth understanding:

  • Each swatch is manufactured under tightly controlled conditions to maintain consistent pigment, gloss, and surface texture.
  • Swatches are periodically reissued because dyes and substrates age, and older chips can drift slightly from the original standard.
  • Fan decks are organized by color family, making it faster to narrow down a shade during buyer discussions.

For textile professionals, these aren’t just color cards — they’re a quality control tool that removes ambiguity from an otherwise subjective process.

Why Pantone Swatches Are Important in the Textile Industry

Color is one of the first things a buyer notices, and it’s also one of the easiest things to get wrong across a long supply chain. A single garment order might pass through yarn dyeing, fabric processing, printing, and finishing — with different vendors handling each stage. Without a common reference, small variations accumulate.

This is where Pantone swatches earn their place on the lab table. They allow a merchandiser to communicate a shade requirement precisely, without relying on descriptive terms like “slightly darker navy” that mean different things to different people.

In day-to-day production, Pantone swatches are used to:

  • Finalize shade approval before bulk dyeing begins
  • Communicate color requirements between buying houses, mills, and dye units
  • Reduce disputes during fabric inspection and shipment approval
  • Maintain color consistency across multiple production lots and even multiple factories

For textile exporters working with international brands, this consistency isn’t optional — it’s often written directly into the buyer’s technical specification sheet, alongside acceptable color difference tolerances.

Understanding Pantone Color Standards

Pantone Color Standards refer to the codified, numbered shades within the Pantone system that serve as the “single source of truth” for a color. When a buyer specifies Pantone 18-1664 TPX for a garment, that code becomes the benchmark against which every dyed lot is measured.

This matters because human color perception is unreliable and highly dependent on lighting. A shade can look acceptable under fluorescent light and noticeably different under daylight or LED — a phenomenon known as metamerism. Pantone color standards, when viewed under controlled lighting conditions in a proper light booth, remove much of that inconsistency.

In practice, textile laboratories typically pair Pantone standards with:

  • A calibrated light source (D65 daylight simulation is the most common reference)
  • A spectrophotometer or colorimeter to measure Delta E (color difference)
  • Documented tolerance limits agreed upon with the buyer

Organizations such as ISO and AATCC publish testing methods that many labs reference for color fastness and evaluation procedures, which work alongside Pantone standards rather than replacing them. Together, these tools form the backbone of a defensible, repeatable color approval process.

Step-by-Step Guide to Using Pantone Swatches for Fabric Color Matching

Here’s how the process typically plays out on a production floor or in a textile laboratory:

Step 1: Receive the color requirement. The buyer or design team specifies a Pantone code, either from a TCX cotton swatch or TPG paper swatch, depending on what was agreed upon in the technical pack.

Step 2: Match the lab dip. The textile lab prepares sample dyeing (lab dips) attempting to replicate the specified Pantone shade on the actual fabric substrate.

Step 3: Evaluate under controlled lighting. The lab dip and the Pantone swatch are compared side by side inside a colour matching cabinet or light booth, typically under D65 daylight, TL84, and sometimes UV or incandescent light sources to check for metamerism.

Step 4: Measure Delta E. A spectrophotometer quantifies the color difference between the lab dip and the standard. Most buyers set a tolerance, commonly around Delta E 1.0, though this varies by fabric type and buyer specification.

Step 5: Get buyer approval. Once the lab dip falls within tolerance, it’s sent for buyer approval, often as a physical swatch card with lot details attached.

Step 6: Scale to bulk production. After approval, the dye recipe is scaled up for bulk production, with periodic checks against the approved standard to catch batch-to-batch drift.

Step 7: Final fabric inspection. Before shipment, finished fabric rolls undergo fabric inspection to confirm the shade still matches the approved Pantone reference.

Common Mistakes to Avoid During Fabric Color Matching

Even experienced production teams run into avoidable errors. The most frequent ones include:

  • Comparing swatches under poor or inconsistent lighting — natural window light, mixed bulb types, or dim workspaces all distort perceived color.
  • Using worn or faded Pantone swatches — physical chips degrade with handling and UV exposure over time, so outdated swatch decks can mislead the entire approval process.
  • Skipping the light booth check — relying only on visual comparison under one light source ignores metamerism, which can cause approved shades to look wrong once the buyer inspects them under different conditions.
  • Ignoring fabric-specific dye behavior — the same Pantone code can behave differently on cotton, polyester, or blended substrates, so lab dip trials shouldn’t be skipped even for “familiar” shades.
  • Not documenting tolerance limits clearly — vague verbal agreements about acceptable color difference lead to disputes later during fabric inspection or shipment.

Avoiding these issues comes down to discipline: consistent lighting conditions, well-maintained equipment, and clear documentation at every stage of the color approval process.

Pantone Swatches vs Digital Color Matching

Digital color matching tools have grown more common, especially with the rise of remote buyer-vendor relationships. But physical Pantone swatches and digital references serve different purposes, and most experienced labs use both.

Aspect Pantone Swatches (Physical) Digital Color Matching
Accuracy on fabric surface High — reflects actual texture, gloss, and dye behavior Limited — screen colors vary by device and calibration
Consistency across locations Very high, as long as swatches are genuine and unfaded Depends on monitor calibration at each end
Speed of communication Requires physical shipping of swatch cards Instant, useful for early-stage discussions
Best use case Final shade approval, bulk production reference Initial concept sharing, remote pre-approval
Cost over time One-time investment in genuine swatch books Ongoing calibration and software costs
Regulatory/spec compliance Widely accepted in buyer tech packs Increasingly used but less standardized industry-wide

In practice, digital tools are excellent for early conversations — sharing a rough color direction over email before samples are even cut. But when it comes to final shade approval and bulk production sign-off, physical Pantone swatches, evaluated under a proper light booth, remain the industry standard. Screens simply can’t replicate how a dye interacts with fabric texture the way a physical swatch can.

Best Practices for Maintaining Color Accuracy

Maintaining consistent color accuracy across seasons and production cycles takes more than owning a swatch book. A few practices separate labs that consistently pass buyer approval from those that struggle:

  • Store swatches away from direct sunlight and humidity, since UV exposure and moisture both accelerate fading.
  • Replace swatch decks periodically, following Pantone’s recommended refresh cycles rather than using the same book for years.
  • Standardize your light booth settings across all vendors in your supply chain, so a mill and a buying house are always comparing shades under identical light sources.
  • Calibrate spectrophotometers regularly to keep Delta E readings reliable.
  • Train staff on visual assessment techniques, since even with instruments, human evaluation remains part of the final sign-off.
  • Maintain a shade approval log documenting lot numbers, tolerances, and sign-off dates for traceability.

These habits reduce rework, shorten approval timelines, and build trust with buyers who audit color consistency across repeat orders.

Industries That Depend on Pantone Swatches

While textiles are a major user base, Pantone swatches support color communication across several connected industries:

  • Apparel manufacturing — garment factories rely on swatches for trims, buttons, zippers, and fabric coordination.
  • Fashion industry and design houses — designers reference Pantone’s seasonal color forecasts when planning collections.
  • Textile exporters — shade consistency across export lots is often a contractual requirement.
  • Buying houses — act as the communication bridge between international brands and local manufacturing units, using swatches to convey buyer expectations precisely.
  • Home textiles and upholstery — bedding, curtains, and furnishing fabrics also depend on consistent color matching.
  • Printing and packaging — brand colors on hangtags, labels, and packaging often need to align with the garment’s Pantone reference.

This cross-industry adoption is exactly why Pantone has remained the default color language for decades — it works the same way regardless of which part of the supply chain you sit in.

How Pantone Swatches Improve Textile Quality Control

Color consistency is a core part of textile quality control, alongside strength, shrinkage, and fastness testing. Pantone swatches feed directly into this process by giving quality teams a fixed benchmark to test against at multiple checkpoints:

  • During lab dip approval, before any bulk dyeing begins
  • At bulk dyeing stage, to catch batch variation early
  • During in-line fabric inspection, to confirm the shade holds through processing and finishing
  • At final audit, before goods are packed for shipment

Textile laboratories that integrate Pantone-based checks at each of these stages typically catch shade deviations early, when they’re cheap to fix, rather than after an entire lot has already been dyed. This is particularly important for garment manufacturing units running high-volume orders, where even a small shade drift across a large batch can result in significant rejected stock.

Choosing Genuine Pantone Color Products

Not all swatch books in the market are genuine, and counterfeit or reproduced Pantone products are a real problem in price-sensitive markets. Using unauthorized copies can be worse than not having a reference at all, since inaccurate pigments lead to incorrect shade approvals that only surface after bulk production.

When sourcing Pantone Color Products for your lab, look for:

  • Official Pantone licensing and authentic packaging
  • Clear batch or edition information printed on the product
  • Supplier reputation within the textile testing equipment industry
  • Compatibility with your existing color matching cabinet or light booth setup

Genuine swatches cost more upfront, but the cost of a single rejected export shipment due to a mismatched shade almost always outweighs the price difference.

Why Buy Pantone Swatches from Amith Garment Services

Amith Garment Services works closely with textile manufacturers, exporters, and buying houses across India’s garment manufacturing hubs, and understands the operational pressure that comes with tight buyer deadlines and strict shade tolerances. The Pantone color products available through Amith Garment Services are sourced to meet the accuracy and consistency that textile laboratories depend on for day-to-day shade approval work.

Beyond swatches themselves, Amith Garment Services also supplies complementary textile testing equipment — including color matching cabinets, light booths, and fabric inspection machines — so labs can build a complete, standardized color evaluation setup rather than piecing together equipment from multiple sources with inconsistent calibration standards.

If your lab is currently relying on outdated or unverified swatch books, it’s worth reviewing your current setup against genuine Pantone color standards before your next buyer audit.

Conclusion

Accurate fabric color matching isn’t a one-time task — it’s an ongoing discipline that touches every stage of production, from the first lab dip to the final shipment inspection. Pantone Swatches remain the most reliable way to keep that discipline consistent, because they give everyone in the supply chain — dyers, quality managers, merchandisers, and buyers — the same physical reference point to work from.

Whether you’re running a textile laboratory, managing quality for a garment exporter, or sourcing on behalf of a buying house, investing in genuine, well-maintained Pantone swatches pays for itself many times over in reduced rework and fewer rejected shipments. Explore the range of authentic Pantone color products and supporting textile testing equipment available at Amith Garment Services to strengthen your shade approval process.

Frequently Asked Questions

Pantone Swatches are used throughout the textile production process to establish, communicate, and verify color accuracy. They serve as the standard reference during lab dip approval, bulk dyeing, and final fabric inspection. Merchandisers use them to specify exact shades, while quality teams ensure dyed fabrics match buyer-approved colors before shipment. Since Pantone codes are recognized worldwide, they eliminate confusion between manufacturers, buying houses, and international brands.

Pantone Swatches provide highly accurate color matching when used under controlled lighting with properly maintained swatch books. For the best results, compare fabric samples inside a colour matching cabinet or light booth using standardized lighting such as D65 daylight simulation. Many textile laboratories also use spectrophotometers to measure Delta E values for precise color evaluation.

TCX (Textile Cotton eXtended) swatches are produced on real cotton fabric, making them ideal for textile dyeing and final shade approval. TPG (Textile Paper Green) swatches are printed on paper, offering a cost-effective solution for initial color selection and design discussions. Most textile manufacturers use TPG for early color planning and TCX for production approval.

Genuine Pantone Color Products should be purchased from trusted suppliers specializing in textile testing equipment. Amith Garment Services supplies authentic Pantone Color Standards along with light booths, colour matching cabinets, and other textile testing solutions for manufacturers, exporters, and buying houses across India.

Pantone Swatches are used to identify and communicate exact fabric colors during textile production. They provide a standardized reference that helps manufacturers, dye houses, and buyers achieve consistent color matching before bulk production begins.

Compare your dyed fabric sample against the corresponding Pantone Swatch under standardized lighting in a light booth or colour matching cabinet. If required, verify the color difference using a spectrophotometer and obtain buyer approval before proceeding with bulk dyeing.

Pantone Color Standards provide a universal color language for the textile industry. They reduce color communication errors, improve consistency between dye houses and buyers, and help maintain uniform shades across the entire textile supply chain.

You can buy genuine Pantone Color Products from Amith Garment Services. The company supplies authentic Pantone color standards along with professional textile testing equipment to textile manufacturers, exporters, and buying houses across India, including Bangalore and Tiruppur.