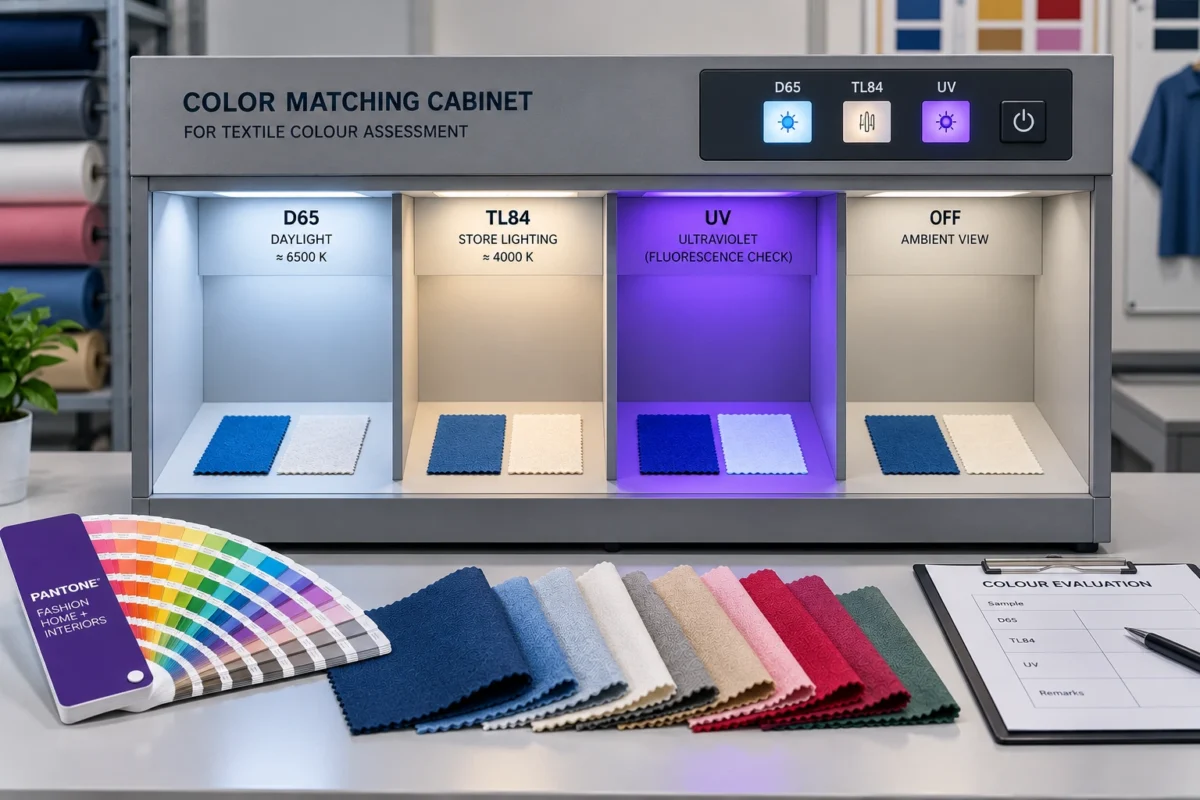
Color Matching Cabinet with D65, TL84 and UV light sources for textile colour assessment

D65, TL84 and UV Light Sources: What Is the Difference?

A fabric is approved in the lab, shipped to the buyer, and suddenly looks different under shop lighting. Anyone in garment manufacturing has seen this. A navy that looks right near a window can turn greyer under office tubes, and a white shirt can glow under UV in ways nobody expected. Often the cause is the light, not the fabric. That is why textile exporters, garment factories and testing laboratories across India, from Bangalore to Tiruppur, assess colour inside a Color Matching Cabinet, where illumination is controlled and repeatable.

What Is a Color Matching Cabinet?

Also called a colour matching light booth, it is an enclosed viewing cabinet fitted with standardised light sources and a neutral interior. It lets technicians compare fabric, trims and garments against an approved standard under controlled illumination instead of whatever room lighting happens to be available.

Room light changes with the time of day, window position and lamp age. Those shifts affect visual judgement. A colour matching cabinet fixes the lighting, and its neutral interior reduces the influence of surrounding colours.

It is a viewing tool, not a guarantee. Results still depend on the observer, the material and the procedure followed.

Why Are Different Light Sources Used for Colour Matching?

No single light represents every viewing condition. Textiles are seen in daylight, shops, offices and sometimes under UV, and colours can shift between them. Laboratories check samples under several light sources to catch differences that one illuminant alone would hide.

Every source spreads its energy across wavelengths differently. Fabric reflects that energy in its own way, so appearance changes with the light. This is the root of metamerism. Checking daylight simulation, retail lighting and UV illumination gives a fuller picture than any one source.

What Is D65 Light Source?

D65 is a CIE standard illuminant that represents average daylight, with a correlated colour temperature of about 6500 K. In textile colour assessment, a D65 light source simulates daylight so technicians can compare fabric and garment colour against approved standards under controlled conditions.

D65 is not identical to natural sunlight, which varies with hour, season and sky. It is a defined reference, and cabinet lamps approximate it as artificial daylight. How closely they match depends on the lamp and system, so check the manufacturer’s specifications.

Colour temperature also describes only the overall tone of the light. Two lamps can both be rated near 6500 K and still render the same fabric differently, because their spectral characteristics differ.

What Is TL84 Light Source?

TL84 is a commonly used reference for commercial store lighting, based on a narrow-band fluorescent lamp with a colour temperature near 4000 K. Buyers use TL84 lighting to see how fabrics and garments may look under typical retail conditions.

TL84 began as a commercial lamp designation, so it is not a CIE standard illuminant like D65. It is often compared with the CIE F11 fluorescent series. Exact specifications vary by lamp and cabinet, so treat 4000 K as approximate. If a buyer names TL84 in their requirements, confirm which lamp they mean.

What Is a UV Light Source?

UV illumination in a colour matching cabinet reveals fluorescence. It mainly shows whether fabrics contain optical brightening agents, which absorb ultraviolet radiation and emit visible blue light. That is why white and pastel fabrics can look different under UV-containing light.

Many white and pastel textiles are treated with optical brighteners. Under a source with UV content they glow, and without it they look duller. UV assessment is therefore a fluorescence check, not ordinary visible-light colour matching. Some D65 simulators include UV content and others do not, so know what your cabinet provides.

D65 vs TL84 vs UV Light Source

D65 simulates daylight at about 6500 K, while TL84 represents retail fluorescent lighting at about 4000 K. Colours look cooler under D65 and warmer under TL84. UV is different: it is not a viewing condition but a way to detect fluorescence.

Feature D65 TL84 UV
Main purpose Daylight assessment Retail-light assessment Fluorescence check
Typical application Shade approval Buyer store-light check Whites, pastels
Approx. colour temperature ~6500 K ~4000 K Not applicable
Represents Standard daylight illuminant Commercial store lighting Ultraviolet radiation
Useful for Matching to standards Spotting retail shifts Detecting brighteners
UV component Varies by cabinet Usually minimal Primary feature
Common textile use Colour approval Garment and buyer checks Optical brightener checks

Values are approximate and vary by lamp and system.

Why Metamerism Matters in Textile Colour Matching

Metamerism is when two samples appear to match under one light but differ under another. It happens because their spectral reflectance curves differ, even though they look alike under the first illuminant. In textiles, it often arises when different dye combinations are used.

Imagine a bulk fabric that matches its standard under D65 but shows a visible difference under TL84. That can mean a rejected shipment. Exporters, garment manufacturers, buying houses, quality teams and merchandisers all share that risk. Checking multiple illuminants helps flag potential metameric pairs early, and instrumental measurement can support the visual check.

How a Color Matching Cabinet Helps Textile Laboratories

In a textile laboratory, a Color Matching Cabinet gives technicians controlled lighting and a consistent place to compare fabric against standards. It suits garments and trims as well, and it allows evaluation under multiple illuminants. That supports quality-control decisions and reduces dependence on changing room light.

Visual assessment should always follow the relevant laboratory or customer procedure, including ISO and AATCC practices where they apply.

D65, TL84 and UV: Which Light Should You Use?

There is no single best light. The choice depends on customer requirements, product application, export market, retail environment, material, the colour standard, laboratory procedure and the presence of optical brighteners.

A shirt for a European retailer may need D65 and TL84 checks. White sportswear may also need a UV check. Always start with the buyer’s written requirements.

Industries That Use Color Matching Cabinets

Beyond textile manufacturing, garment manufacturing and dyeing and finishing, they are common in export houses, buying houses, fabric testing laboratories and home textiles. Fashion and apparel teams use them, and printing and packaging sometimes do too. In India, Tiruppur’s knitwear exporters and Bangalore’s garment manufacturers regularly work to buyer-specified lighting. Quality-control departments use the cabinet daily for colour evaluation and textile inspection.

How to Choose the Right Color Matching Cabinet

Consider these points before buying:

  • Light sources: which of D65, TL84 and UV you actually need
  • Number of illuminants: match it to buyer requirements
  • Light uniformity across the viewing area
  • Interior surface and viewing environment
  • Lamp replacement availability, and a timer or hour meter
  • Colour evaluation needs and available laboratory space
  • Manufacturer specifications: ask for lamp data
  • Calibration and maintenance expectations
  • Compliance with customer or laboratory procedures

Why Choose Amith Garment Services for Textile Testing Equipment?

Amith Garment Services supplies textile testing equipment for garment and fabric laboratories. The range includes the colour matching cabinet, crock meter for colour fastness testing, washing fastness tester, GSM cutter, fabric inspection machine, bursting strength tester and fabric rolling machine.

These instruments cover practical quality-control needs in garment manufacturing and textile laboratories. The team can discuss your testing requirements and help you select suitable equipment. Confirm specifications against your own procedures before purchase.

Conclusion

D65 simulates daylight, TL84 represents common store lighting, and UV reveals fluorescence from optical brighteners. Each shows a different side of colour appearance, which is why they are not interchangeable. Used with the right procedure, a Color Matching Cabinet gives textile teams consistent, controlled conditions for colour evaluation, though it works best alongside trained observers and, where needed, instrumental measurement.

Frequently Asked Questions

A Color Matching Cabinet is used to assess fabric, trim and garment colour under controlled, repeatable lighting. Technicians compare a production sample with an approved standard under sources such as D65, TL84 and sometimes UV, away from changing room light. This helps textile laboratories, garment factories and buying houses make more consistent visual decisions. It does not replace instrumental measurement, and results still depend on the observer, material and the relevant customer or laboratory procedure.

D65 is a CIE standard illuminant that represents average daylight at roughly 6500 K, so it is used to judge colour under daylight-like conditions. TL84 is a commercial fluorescent reference associated with store lighting, with a colour temperature near 4000 K. D65 shows how a colour behaves in daylight, while TL84 shows how it may look in a shop. Exact specifications vary by lamp and cabinet, so always check the manufacturer's data.

UV light is used to reveal fluorescence, mainly in fabrics treated with optical brightening agents. These agents absorb ultraviolet radiation and re-emit it as visible blue light, making whites and pastels look brighter. Checking under UV helps technicians see whether two samples contain different levels of brightener, which could cause a visible mismatch under certain lighting. It is a fluorescence check rather than a replacement for visible-light colour matching.

Yes. This is called metamerism. Two samples can have different spectral reflectance, such as when different dye combinations are used, yet look identical under one illuminant. Under another light with a different spectral distribution, such as TL84, the difference may become visible. That is why laboratories check important shades under more than one light source before approving a lot or shipping to a buyer.

It's a viewing cabinet with standard lights that lets you compare fabric colours under controlled lighting. Textile labs and garment factories use it to check a sample against an approved standard without room lighting changing the result.

D65 is a standard daylight reference at about 6500 Kelvin. In a colour matching cabinet, it simulates daylight so you can judge how a fabric colour compares with its approved standard.

TL84 is a commonly used store-lighting reference at around 4000 Kelvin. Buyers and garment makers use it to see how a fabric or garment colour will look under typical shop lighting.

They use UV light to spot fluorescence, especially from optical brighteners in white and pastel fabrics. It shows whether a fabric glows under ultraviolet, which can change how it looks under some lighting.
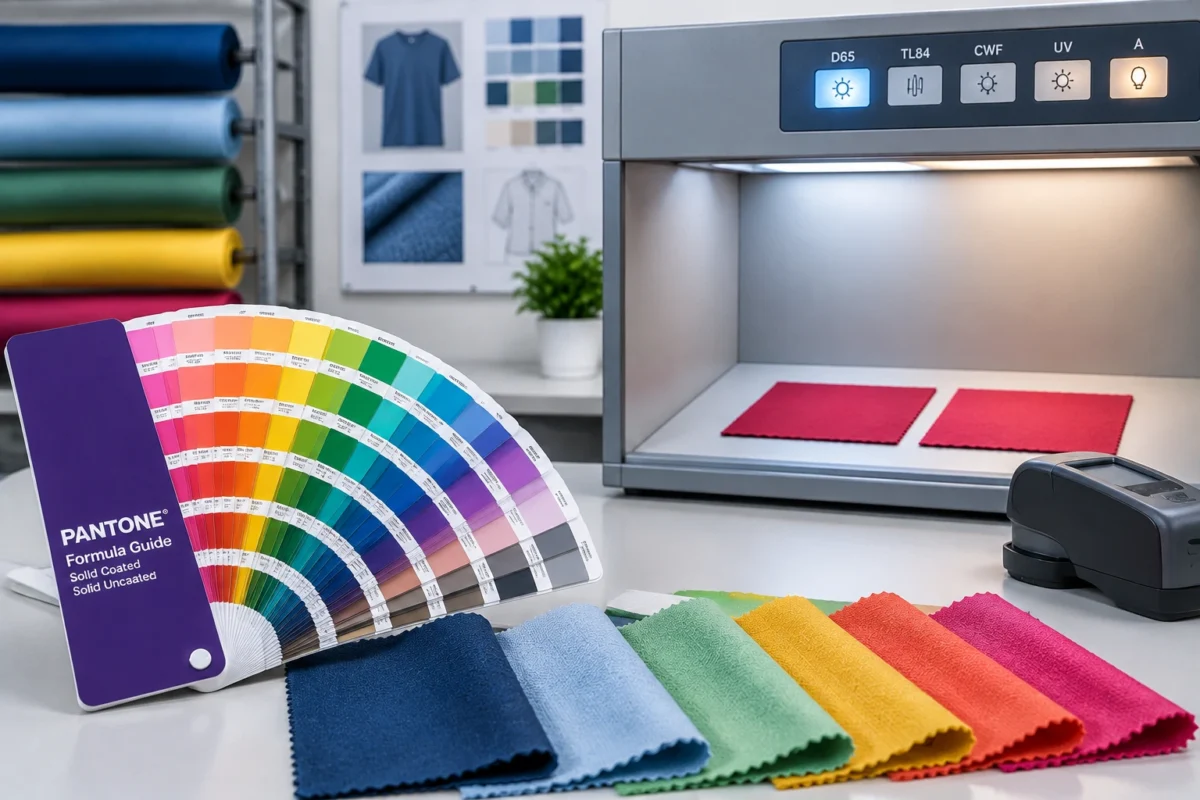
Pantone Color Standards used for textile colour matching and quality control

What Are Pantone Color Standards and Why Are They Important?

What Are Pantone Color Standards?

Pantone Color Standards are the standardized colour references built around the Pantone Color System, where each shade carries its own identifier. A name like “sky blue” is open to interpretation. A code is not.

For textiles, designers typically cite codes from Pantone’s fashion and home range, often supplied as cotton-based swatches (TCX). Manufacturers then treat that code as the target during development, lab dipping and production.

Pantone Color Standards are standardized, coded colour references that let designers, buyers and manufacturers specify the same shade without relying on subjective names. Each colour has a unique identifier, which reduces misunderstandings during development, sampling and production, especially across suppliers and countries.

Why Are Pantone Color Standards Important in Textile Manufacturing?

Colour is usually the first thing a buyer notices and the first reason a shipment is questioned. A shared reference helps at every stage: fabric development, sampling, dyeing, printing, bulk production, buyer approvals and export documentation.

Picture a knitwear order. The buyer sends a code, the mill dyes a lab dip, and the garment factory cuts panels from two dye lots. Without a common reference, each party judges “close enough” differently. With one, the disagreement becomes a discussion about measurable deviation rather than opinion.

Why are they important? They give everyone in the supply chain the same colour target. That reduces sampling rounds, limits shade disputes, supports buyer approvals and makes quality control more objective across fabric, printing and garment production.

How Do Pantone Color Standards Work?

The usual workflow looks like this:

  1. The buyer or designer selects a colour reference.
  2. The code is communicated to the manufacturer.
  3. Lab dips or fabric samples are prepared.
  4. Colour is evaluated under controlled lighting.
  5. Recipes are adjusted where necessary.
  6. The approved shade becomes the production reference.
  7. Bulk production is checked against that approved standard.

How are Pantone colours used in textiles? Designers cite a code in the tech pack, mills and dyeing units use it as the lab-dip target, and quality teams compare bulk fabric or garments against the approved shade under controlled light.

One caution: the same code will not look identical on every material. Fibre type, dye chemistry, fabric construction, finishing, surface texture, printing method and viewing conditions all shift appearance. A Pantone reference is a target, not a guarantee of an exact physical match on every substrate.

Pantone Color Standards vs Pantone Colour Guides

The two terms are often used interchangeably, but they play different roles. Broadly, the standards are the coded colour references. The guides are the tools that present them.

Factor Pantone Color Standards Pantone Colour Guides
Purpose Define and codify reference colours Present those colours as physical or digital swatches
Colour Reference The coded shade identity A printed or dyed representation of it
Manufacturing Use Target for development and approval Visual aid in the office, lab or floor
Textile Application Specifying fabrics, trims and garments Substrate-specific guides (e.g., cotton) for selection
Quality Control Basis for deviation checks Visual comparison only; sensitive to light and ageing
Buyer Communication Codes in tech packs and approvals Shows intent alongside the code

Pantone offers several systems and formats, and the Pantone Matching System (PMS) is best known in print. Always confirm which one your buyer specifies.

Why Is Pantone Colour Matching Important for Fabrics?

Pantone colour matching links design intent to real cloth. It shapes shade development, lab dips, dyeing, fabric inspection, buyer approval and shade consistency in bulk.

What is Pantone colour matching? It is the process of adjusting a dye or print recipe until a fabric sample aligns with a chosen Pantone reference within an agreed tolerance, usually checked under standardized lighting before buyer approval.

Ordinary office light or window daylight is a poor judge. Both change through the day and with the weather. Controlled lighting gives every evaluator the same conditions, so a disagreement reflects the fabric, not the room.

Role of a Color Matching Cabinet in Pantone Colour Evaluation

A Color Matching Cabinet, also called a light booth, provides standardized light sources inside a neutral enclosure. Common options include daylight simulation, TL84 store lighting, and incandescent or UV sources.

Why several? Metamerism. Two samples can match under one illuminant and visibly differ under another, often because different dyes were used. Checking under multiple sources exposes this before the buyer does. This textile laboratory equipment lets mills, factories and buyers compare shades under the same conditions.

What is the difference between Pantone and a colour matching cabinet? Pantone supplies the colour reference; the cabinet supplies the lighting to judge it. One defines the target, the other standardizes how you view the target and the sample.

Why is controlled lighting important? Colour appearance changes with the light source. Standardized illuminants and neutral surroundings let evaluators compare shades consistently and reveal metamerism, so decisions don’t depend on time of day, weather or room.

Pantone Color Standards and Textile Quality Control

Standardized references support quality control at each checkpoint:

  • Incoming fabric inspection: confirming supplied fabric against the reference
  • Lab dip approval: documenting the accepted shade
  • Production monitoring: catching drift between dye lots
  • Shade grouping: keeping panels from the same garment visually consistent
  • Final inspection and buyer approval: verifying against the signed-off standard

Colour consistency shapes perceived quality. A sleeve slightly off from the body panel reads as a defect, even when every strength test passes.

Factors That Can Affect Colour Matching

  • Fibre and construction: the same dye looks different on cotton, polyester or a textured knit.
  • Dye selection and concentration: small recipe changes shift the shade.
  • pH, temperature and processing time: a bath that runs slightly hotter or longer can change results.
  • Finishing: softeners and resin finishes may alter depth or tone.
  • Viewing conditions: lighting, viewing angle and surface gloss change perception.
  • Instrument calibration and sample preparation: uncalibrated devices or unevenly conditioned samples give misleading comparisons.

Pantone Color Standards in Garment Exporting

International buyers often specify colours by code, and Indian manufacturers, dyeing houses and fabric suppliers work from the same reference. In hubs such as Tiruppur, where knitwear exporters manage large repeat orders, and in Bangalore’s garment manufacturing sector, that shared reference helps keep shade expectations aligned across the textile industry. For textile exporters, a documented approved standard also makes it easier to resolve questions after shipment.

How to Maintain Better Colour Consistency in Textile Production

  • Use a defined colour reference for every order.
  • Keep approved lab-dip standards on file.
  • Evaluate shades under controlled lighting.
  • Hold dyeing and finishing parameters steady.
  • Calibrate relevant instruments.
  • Compare bulk production with the approved sample.
  • Record shade deviations and maintain testing documentation.
  • Train quality-control personnel.

Distinguish the two assessment methods. Visual assessment relies on trained observers under standard light. Instrumental measurement uses a spectrophotometer to quantify colour difference numerically. Most laboratories use both, and both are commonly guided by AATCC and ISO practices.

Choosing the Right Textile Colour Testing Equipment

Consider the application, testing requirements, lighting needs, compatibility with the standards your buyers use, and how the equipment fits your laboratory workflow. Then look at repeatability, calibration, ease of operation, maintenance, documentation and production volume. A small sampling unit and a large export facility may need very different textile testing equipment. Garment testing instruments for colour should sit alongside those for fastness and physical properties, not in isolation.

Why Choose Amith Garment Services?

Amith Garment Services provides textile testing equipment and related solutions for textile and garment quality-control applications. The range relevant to colour and fabric evaluation includes the Color Matching Cabinet, Crock Meter, Washing Fastness Tester, GSM Cutter, Fabric Inspection Machine, Bursting Strength Tester and Fabric Rolling Machine. Together, these help laboratories check colour, fastness and physical properties in one workflow. For advice on matching equipment to your testing requirements, contact the team through the website.

Conclusion

Pantone Color Standards turn subjective colour talk into a shared, documented reference that suits the realities of textile manufacturing. They work best when combined with lab dips, controlled lighting, calibrated instruments and disciplined records. Used that way, they help mills, factories and exporters deliver colour their buyers expect.

Frequently Asked Questions

Pantone Color Standards are used to specify, communicate and verify colour throughout textile production. Designers cite a code in the tech pack, mills and dyeing units use it as the target for lab dips, and quality teams compare bulk fabric or finished garments against the approved shade. Because the reference is coded rather than described in words, it cuts down on misinterpretation between buyers, factories and suppliers. It works best when paired with controlled lighting and, where required, instrumental colour measurement.

Pantone colour matching gives garment manufacturers a clear target from the first sample. Merchandisers can brief the dyeing unit with a code instead of a vague description, which can shorten lab-dip rounds and reduce shade disputes at approval. During production, the approved standard lets quality teams judge whether dye lots and panels stay within tolerance. It also supports smoother communication with international buyers, who often specify colours by code, though the final match still depends on the fabric and process.

Not always. A Pantone reference is a colour target, but fabrics respond differently to dyes and finishes. Fibre type, yarn and fabric construction, dye class, finishing and surface texture all influence how a shade appears, so a colour achieved on cotton may look different on polyester or a textured knit. Some colours may also fall outside what a given dye system can reproduce. Manufacturers therefore prepare lab dips, evaluate them under standardized light, and agree tolerances with the buyer rather than assuming an identical match.

A Color Matching Cabinet provides standardized, repeatable lighting so shade comparisons don't depend on the time of day, weather or room. Most offer several light sources, such as daylight, store lighting, and incandescent or UV, which helps reveal metamerism, where samples match under one light but not another. Using the same conditions at the mill, the factory and the buyer's office makes Pantone Color Standards easier to apply consistently. It supports visual assessment but does not replace instrumental measurement when numerical data is required.

They define and communicate colour with a code instead of a description. In textiles, buyers and manufacturers use them to agree on a shade, prepare lab dips, and check bulk production against the approved colour.

First, the buyer picks a Pantone code. The mill prepares lab dips to match it, and the shade is checked under controlled lighting. Once approved, that sample becomes the production standard, and bulk fabric is compared against it.

Because a code means the same thing to everyone. Instead of arguing over what "olive green" means, buyers, dyeing units and garment factories work from one reference, which cuts down on shade misunderstandings and rework.

Place the fabric and the approved standard side by side in a colour matching cabinet, then view them under standard light sources such as daylight. If needed, confirm with a spectrophotometer to measure the colour difference numerically.