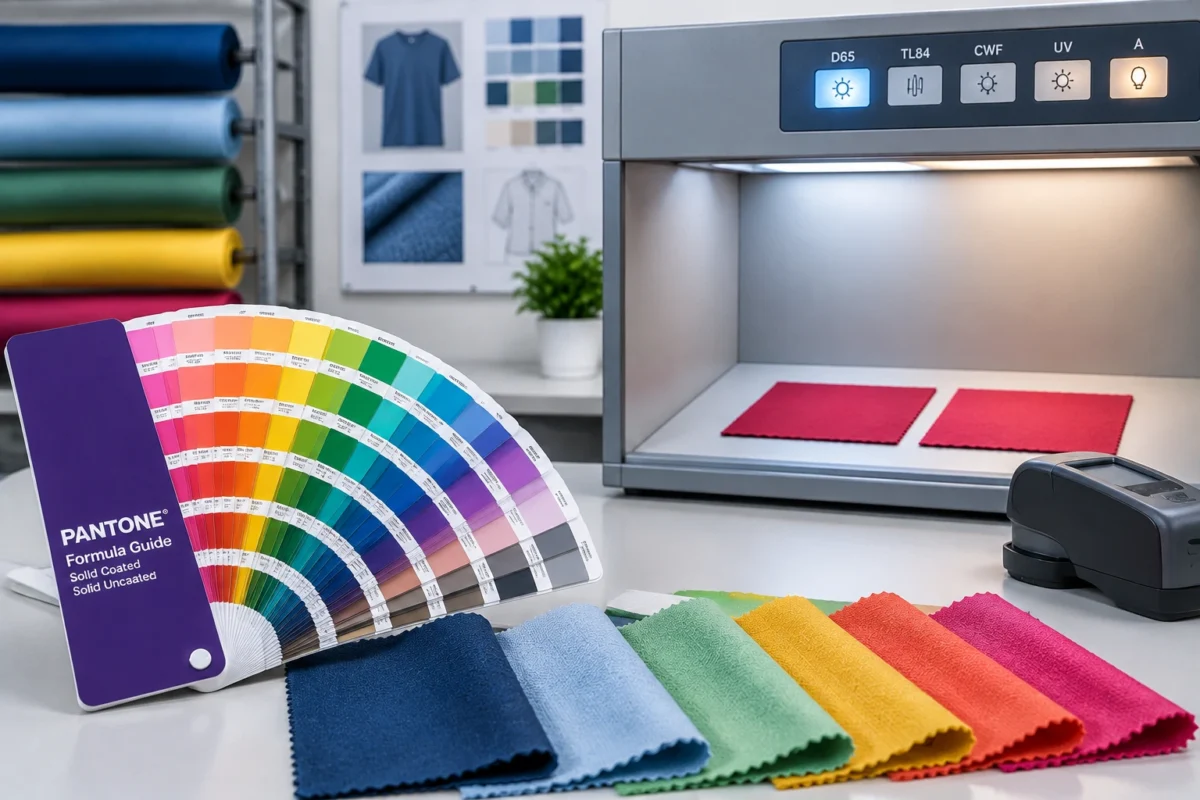
Pantone Color Standards references arranged beside fabric swatches for textile color matching

Pantone Color Standards for Textile Industry: Complete Guide

Pantone Color Standards give textile teams a shared language for color. When a designer, a dyeing unit, a garment factory and an overseas buyer must agree on one shade, a numbered physical reference removes a lot of guesswork. That matters in fabric development, dyeing, garment manufacturing and export quality control. It does not remove variation by itself, so this guide also covers how to use it well.

What Are Pantone Color Standards?

Pantone Color Standards are numbered, named color references that let people specify a target shade without describing it in words. A designer picks a code, the supplier receives the same code, and both compare their work with a physical reference. For textiles, the relevant system is Pantone Fashion, Home + Interiors (FHI).

A reference communicates a target. It does not guarantee an identical match on every fiber, finish or light source.

What are Pantone Color Standards?
Pantone Color Standards are numbered, named color references used to specify and communicate target shades across design, production and approval. In textiles, they give designers, mills, dyeing units and buyers a shared point of comparison, although the match on fabric still depends on material, finish and lighting.

Why Are Pantone Color Standards Important in the Textile Industry?

A shared reference matters most where several parties handle the same color:

  • Specification: one code replaces vague descriptions like “dark navy”.
  • Fabric and yarn development: teams know which shade they are aiming for.
  • Dyeing and finishing: recipes can be built and corrected against a known target.
  • Lab dip approval: buyer and supplier judge submissions against the same reference.
  • Bulk production: the approved standard gives production something to check against.
  • International trade: a code travels across borders more reliably than a verbal description.

This reduces avoidable discrepancies, but it cannot eliminate them. Fiber, dye chemistry and finishing still shape the result.

Why are Pantone Color Standards important in textiles?
They give buyers, mills and garment makers a common reference for specifying, developing and approving colors. This reduces miscommunication during lab dips and bulk production, especially in international sourcing, although fabric composition, dyeing and lighting still influence the final appearance.

Different Types of Pantone Color Guides Used in Textiles

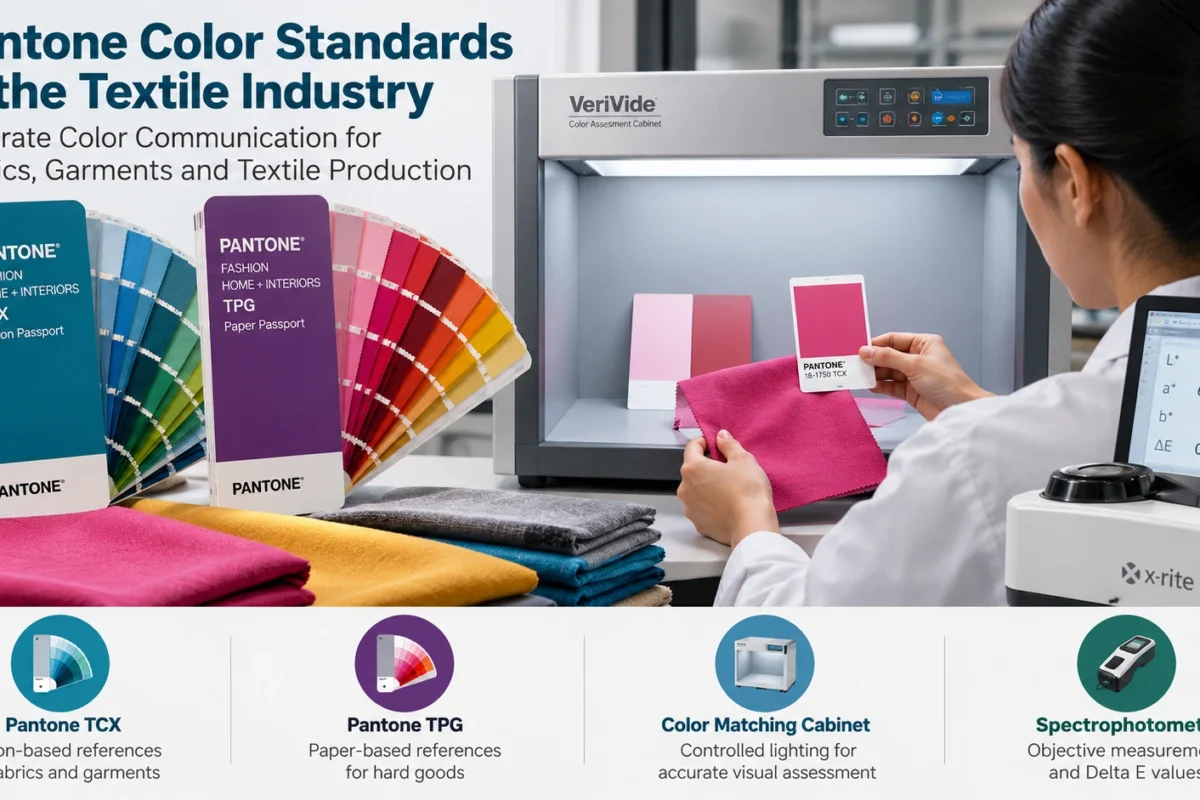
Pantone offers several reference systems, and they are not interchangeable. Within Pantone Fashion, Home + Interiors, TCX references show colors on cotton, while TPG references show the same system as a lacquer on coated paper. Pantone positions TPG for hard goods such as ceramics, paint, cosmetics, accessories and leather, and TPG colors are designed to match back to TCX. The Pantone Formula Guide is a print and graphic design system, so don’t treat it as a textile reference by default.

Pantone Reference General Application Important Consideration
Fashion, Home + Interiors (FHI) Fashion, textiles, interiors Parent system; confirm which format the buyer specifies
TCX (cotton) Fabrics, garments, soft goods Cotton-based, so closest to a textile substrate
TPG (paper) Hard goods, accessories, leather Lacquered paper; matches back to TCX but is a different surface
Formula Guide Graphic design and print Ink on paper; not textile-specific

Always confirm the exact guide, edition and format with your buyer, and check Pantone’s official site for current product names.

What is the difference between TCX and TPG?
TCX references show Pantone FHI colors on cotton, suited to soft goods like fabric and garments. TPG references show the same system on lacquered coated paper, suited to hard goods such as accessories and leather. TPG colors are designed to match back to TCX, but they are different surfaces.

How Pantone Color Standards Work in Fabric Color Matching

A typical workflow looks like this:

  1. Select the reference the buyer specifies.
  2. Send the exact color code to the supplier.
  3. Prepare a lab dip or fabric sample.
  4. Compare the sample against the agreed reference.
  5. Assess it under suitable lighting.
  6. Measure color difference instrumentally when required.
  7. Obtain buyer approval before bulk production.
  8. Run production checks to monitor consistency.

A good lab dip can still look “off” because the standard and your fabric are different materials. Fiber composition, dye chemistry, construction, texture and finishing all change how light reflects, so one color can look different on cotton, polyester or a brushed surface.

How do textile manufacturers match fabric colors to Pantone references?
They receive the specified code, prepare lab dips, and compare them with the physical reference under controlled lighting. Where required, they measure color difference with a spectrophotometer, then seek buyer approval before bulk dyeing and keep checking production batches.

Pantone Color Standards vs. Digital Color Codes

RGB and HEX describe color as light mixed on a screen. A Pantone reference is a physical object seen by reflected light. The same HEX code can look different on two devices, and neither reproduces a dyed fabric exactly.

Aspect Pantone physical reference RGB / HEX
Medium Physical sample Light emitted by a screen
Viewing Reflected light; depends on the light source Depends on device, brightness, calibration
Best use Specification and approval Early design and quick sharing
Limitation Specific to its substrate Cannot represent every textile color

Use screens for early concepts and physical references for approval.

Can a Pantone color look different on fabric and on a screen?
Yes. Screens emit light and vary by brightness and calibration, while fabric reflects light and is affected by fiber, texture and finish. A digital swatch is only an approximation, so approvals should rely on physical references and samples.

The Role of a Color Matching Cabinet and Light Booth

A color matching cabinet, often called a light booth, gives evaluators a controlled environment for visual assessment. Instead of judging a shade near a window or under factory tube lights, they compare the approved reference and the production sample under defined light sources with neutral surroundings.

This matters because of metamerism: two samples can match under one light and differ under another, often because different dyes or pigments were used. Checking under more than one light source exposes this before bulk goes out.

Which illuminants and procedure apply depends on the buyer’s requirements and the relevant test protocol, so follow the buyer’s instruction rather than assuming a default.

Why is a color matching cabinet used in textile quality control?
It provides standardized, repeatable lighting so evaluators can compare fabric samples with approved references fairly. It also helps reveal metamerism, where colors match under one light source but differ under another, before bulk production proceeds.

How Spectrophotometers and Delta E Help with Color Assessment

A spectrophotometer measures the light a fabric reflects across the visible spectrum and converts it into numerical color data. Delta E (ΔE) expresses the difference between two measured colors, such as standard versus sample, as a single number.

What a given ΔE means depends on the color-difference formula, measurement conditions, the material and the buyer’s acceptance criteria. There is no universal limit that suits every fabric or customer, so use the tolerance in the buyer’s specification. Instrument data complements visual assessment rather than replacing it. Numbers are objective and repeatable, while visual checks catch what the end customer will actually see.

Common Challenges in Pantone Color Matching

Typical causes of color variation include:

  • Fiber composition, dye selection and dye concentration
  • Fabric construction and surface texture
  • Dyeing and finishing conditions, and batch-to-batch variation
  • Different lighting, and different instrument settings or measurement conditions
  • Comparing a physical reference with a screen
  • Choosing the wrong reference, such as a print-oriented guide for fabric
  • Weak lab dip approval procedures

Practical fixes: confirm the reference system in writing, fix the lighting and measurement conditions, and agree how many lab dip rounds and which criteria apply.

How to Maintain Color Consistency in Textile Production

  • Use the agreed reference and record the color code, edition and approved sample details.
  • Prepare and evaluate samples the same way every time.
  • Assess under agreed lighting, and add instrumental readings when specified.
  • Document buyer-approved acceptance criteria and every lab dip approval.
  • Monitor bulk dyeing and finishing batches against the approved standard.
  • Report deviations to the buyer before production continues.

A Pantone reference says what the color should be, not how well it will hold up. Rubbing and wash fastness are tested separately with crock meters and wash-fastness testing instruments.

Choosing the Right Pantone Color Products for Your Business

Start with the application. A mill working to a buyer’s TCX specification needs a cotton-based guide, while a team developing accessories may need TPG. Don’t substitute a print-oriented Formula Guide for textile work. Then consider how many colors you need, whether you need physical guides for every desk, how updates and replacements are handled, and whether the guide matches what your buyers specify. Finally, decide whether you also need a color matching cabinet or other testing equipment to evaluate samples consistently.

Pantone Color Standards in India’s Textile and Garment Industry

India’s textile industry spans fabric dyeing and processing through to garment manufacturing. Business and sourcing hubs such as Bangalore and Tiruppur show how many parties may handle one color before it reaches a retailer: textile exporters, processing units, buying house teams and international buyers. When each reads the same code from the same physical reference, fewer shade questions travel back and forth across time zones. Buyer requirements commonly name the reference system and approval steps, so confirm them at the start of an order.

Why Choose Amith Garment Services?

Amith Garment Services is a Bangalore-based supplier of textile testing and quality-control instruments, established in 1999 according to its website. Its range includes Pantone color standards, fabric inspection machines, GSM cutters, crock meters, bursting strength testers and colour fastness testing instruments, along with calibration services. Labs that check color usually also check GSM, rubbing fastness, fabric defects and strength, so planning instruments as one workflow can simplify setup. Explore the Pantone Color Standards page, or contact the team through the website for product information.

Conclusion

Pantone Color Standards help teams communicate target colors and stay coordinated from development to delivery. They work best alongside suitable lighting, documented lab dip approvals and consistent quality-control checks, with instrumental measurement added when the buyer requires it. Put those pieces in place, and your team will get far more from Pantone Color Standards.

Frequently Asked Questions:

1. What are Pantone Color Standards in the textile industry?

Pantone Color Standards are numbered, named color references that help designers, mills, dyeing units, garment manufacturers and buyers agree on a target shade. In textiles, the relevant system is Pantone Fashion, Home + Interiors, which includes cotton-based TCX and paper-based TPG references. A reference communicates the intended color, but the final result on fabric still depends on fiber, dyes, finishing and the lighting used for assessment.

2. What is the difference between Pantone TCX and TPG?

TCX references present Pantone Fashion, Home + Interiors colors on cotton, making them suitable for fabrics, garments and other soft goods. TPG references present the colors on coated paper with a lacquer finish and are intended for hard goods such as ceramics, paint, cosmetics, accessories and leather. TPG colors are designed to match back to TCX, but the surfaces differ, so confirm which format your buyer specifies.

3. How do Pantone references help with fabric color matching?

Pantone references give everyone the same color target. The buyer specifies a code, the supplier prepares a lab dip or sample, and the team compares it with the physical reference under agreed lighting. Where required, a spectrophotometer provides Delta E color-difference measurements. Buyer approval should be obtained before bulk production. The reference supports communication and comparison but cannot guarantee an exact match on its own because fabric and finishing influence color.

4. Which equipment helps assess textile colors accurately?

Visual assessment is usually performed in a color matching cabinet or light booth, which provides controlled lighting for comparing samples with approved references. A spectrophotometer adds objective measurements and Delta E values. Physical Pantone guides provide the color reference, while lab dyeing equipment supports lab dip preparation. The appropriate illuminants, formulas and tolerances depend on buyer requirements and the relevant test protocol.

5. What are Pantone Color Standards used for?

Pantone Color Standards are used to select, describe and approve specific colors. In textiles, they help designers, mills and buyers agree on a shade so everyone works toward the same target during product development and production.

6. How do I match a fabric to a Pantone color?

Start with the Pantone code specified by the buyer. Prepare a lab dip, compare it with the physical reference under controlled lighting, and measure the color difference if required. Obtain buyer approval before starting bulk production.

7. What is the difference between TCX and TPG?

TCX presents Pantone Fashion, Home + Interiors colors on cotton, making it suitable for fabric and garment applications. TPG presents the colors on coated paper and is intended for hard goods such as accessories. Confirm which format the buyer requires before ordering.

8. Which equipment helps check fabric color under standard lighting?

A color matching cabinet, also called a light booth, provides controlled lighting for comparing fabric with a color reference. A spectrophotometer can provide measured color-difference data when required by the buyer or testing procedure.
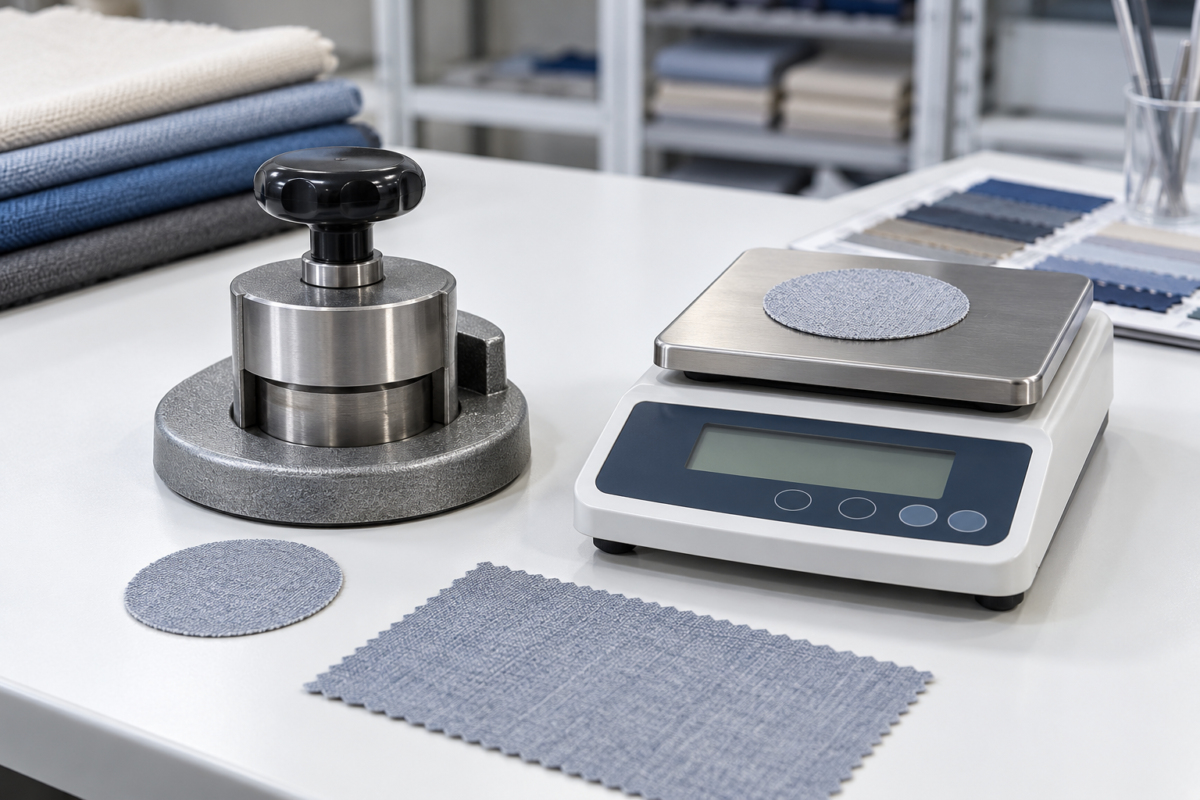
Fabric GSM testing setup with a round GSM cutter and precision weighing balance

How to Measure Fabric GSM Accurately

Fabric GSM, or grams per square metre, is the mass of a fabric in one square metre of area. It influences handfeel, durability, cost and specification matching. For mills, garment manufacturing units and textile exporters, a dependable GSM Machine in Tirupur or anywhere else in India only helps when it is paired with correct sampling, cutting, weighing and calculation.

What Is Fabric GSM and Why Does It Matter?

Fabric GSM means grams per square metre. It states how much a fabric weighs for each square metre of area, helping buyers and quality teams compare fabrics, confirm specifications and check consistency between lots. A higher GSM generally means a heavier fabric, although construction and fibre also decide how it performs.

GSM is not the same as thickness or density. Thickness is the distance through the fabric, usually in millimetres. Density in textile work usually refers to how closely yarns are packed, such as ends and picks in woven fabric or wales and courses in knits. Two fabrics can share the same GSM and still differ in thickness.

Why is GSM important in garment manufacturing? It ties the fabric to the garment specification. GSM affects handfeel, drape, warmth, durability and fabric cost, and measuring it helps teams catch lot-to-lot variation before cutting begins.

How to Measure Fabric GSM Accurately

Take a representative sample, condition it as the test method requires, and cut a specimen of known area. Weigh it on a calibrated balance, divide the weight in grams by the area in square metres, and compare the result with the specification. Repeat on several specimens and record the average.

  1. Select a representative sample. Avoid the outer layers of a roll, creases and selvedge edges.
  2. Condition the sample. Follow the applicable test method, because moisture changes weight.
  3. Use a GSM cutter or an accurately measured specimen. A round cutter gives a fixed area with clean edges.
  4. Confirm the specimen area. Do not assume it; check the cutter’s stated area.
  5. Weigh on a calibrated balance. Readability should suit the specimen’s weight.
  6. Calculate GSM using the formula below.
  7. Compare with the specification and any tolerance agreed with the buyer.
  8. Record the result with units, and repeat measurements where needed.

Each of these factors feeds directly into the final number. The exact procedure depends on the applicable test method and laboratory requirements.

How Does a GSM Machine in Tirupur Help Measure Fabric Weight?

Fabric GSM testing normally needs a GSM round cutter, a precision weighing balance and a way to calculate the result. Some products combine these steps, while others supply only one. Choose the configuration according to your fabric type, testing volume and workflow.

A typical setup includes a cutter and a balance, but “GSM testing machine” covers different configurations, and not every product sold under that name does both jobs.

  • GSM cutters produce specimens of a defined area, commonly 100 cm².
  • Precision balances record specimen weight; readability and calibration drive accuracy.
  • GSM calculator machines or digital calculators speed up the arithmetic.

How can a GSM Machine in Tirupur support fabric quality control? A well-chosen GSM setup in a Tiruppur unit makes incoming fabric checks quick and repeatable. Consistent specimen areas and calibrated weighing let teams compare lots, spot deviations early and keep records for buyer discussions. Regular calibration and correct operation remain essential.

GSM Calculation Formula With a Practical Example

GSM = specimen weight in grams ÷ specimen area in square metres. If a 100 cm² specimen weighs 1.8 g, convert the area to 0.01 m² and divide: 1.8 ÷ 0.01 = 180 GSM.

Item Value
Specimen weight 1.8 g
Specimen area 100 cm² = 0.01 m²
Calculation 1.8 g ÷ 0.01 m²
Final result 180 GSM

Since 1 m² equals 10,000 cm², 100 cm² is 0.01 m². For a 100 cm² specimen, you can multiply the weight in grams by 100 as a shortcut.

This result is only as good as the specimen area and the weighing. A GSM calculator machine or calculator automates the arithmetic, but it cannot fix inaccurate cutting, weighing or sampling.

Common Mistakes to Avoid When Measuring Fabric GSM

  • Wrong specimen area: a worn or mismatched cutter shifts every result.
  • Irregular or damaged specimens: frayed or distorted edges change weight and area.
  • Uncalibrated balance: drift produces consistently wrong values.
  • Ignoring conditioning: moisture can raise or lower weight.
  • Testing one unrepresentative piece: a single cut rarely reflects a roll.
  • Confusing thickness with GSM: a thick fabric is not necessarily a heavy one.
  • Recording wrong units: mixing grams, milligrams, cm² and m² causes large errors.
  • Using unsuitable equipment: a cutter or balance mismatched to the material limits repeatability.

These errors can cause wrongly accepted or rejected lots and buyer disputes.

GSM Testing Machine vs GSM Calculator Machine

A GSM testing machine or setup prepares and weighs the specimen, usually through a cutter and balance. A GSM calculator machine only performs the arithmetic once weight and area are known. It cannot cut, weigh or correct sampling errors, so the two are not interchangeable.

Item Main purpose What it does not do
GSM testing machine / setup Specimen preparation and weighing (configuration varies) May not include calculation or calibration records
GSM cutter Cuts a specimen of fixed area Does not weigh
Weighing balance Measures specimen weight Does not cut or calculate GSM
GSM calculator machine / tool Converts weight and area to GSM Does not prepare or weigh specimens

The right configuration depends on whether you need specimen preparation, weighing, calculation or a complete laboratory workflow.

Factors That Affect Fabric GSM Results

  • Construction and yarn: yarn count, twist and structure change fabric mass.
  • Knitted vs woven: knits stretch easily, so cutting without distortion needs extra care.
  • Moisture and conditioning: absorbed moisture adds weight.
  • Sample location: weight can vary across width and along length.
  • Finishing treatments: softeners, coatings and compaction alter mass per area.
  • Specimen size: small specimens magnify errors.
  • Balance resolution and calibration: low resolution limits precision.

Genuine fabric variation shows up as differences between positions or rolls even when the method is controlled. Measurement error shows up as scatter between repeat tests on the same spot or as consistent bias across all results.

Which Standards Are Used for Fabric GSM Testing?

Laboratories should use a recognised method for mass per unit area. Two commonly referenced ones are ISO 3801, which covers mass per unit length and mass per unit area of woven fabrics, and ASTM D3776/D3776M, which covers mass per unit area (weight) of fabric.

The right choice depends on fabric construction, product requirements, customer specifications and laboratory procedures. For knitted fabrics, confirm which method the buyer specifies. Consult the latest official version of the standard, including its conditioning requirements, before formal compliance testing.

Industries That Use a GSM Machine in Tirupur and Across India

GSM measurement supports:

  • Garment manufacturing and knitted and woven fabric production, for matching fabric to specifications.
  • Textile exporters and buying houses, for checking lots against buyer requirements.
  • Fabric testing laboratories, for routine and comparative testing.
  • Home textile production, where fabric weight affects product feel and performance.

Across India’s textile industry, hubs such as Tiruppur and Bangalore combine manufacturing, sourcing and quality assurance activity.

How to Choose the Right GSM Machine in Tirupur

When evaluating a GSM Machine in Tirupur or any GSM testing equipment, consider:

  • Fabric type and specimen requirements
  • Measurement range and required accuracy
  • Cutter size and specimen area
  • Balance capacity and readability
  • Ease of use and maintenance
  • Calibration and documentation needs
  • Availability of accessories
  • Technical support and written product specifications
  • Compatibility with your test procedures

Ask for written specifications and match the equipment to your fabrics and testing volume.

Why Consider Amith Garment Services for Textile Testing Equipment?

Amith Garment Services is a Bangalore-based supplier of textile testing and quality control instruments. Its website states that it was established in 1999 and lists categories including fabric testing equipment, swatch and GSM cutting machines, fabric inspection machines, calibration and repair services, and consultation on choosing instruments.

Suitable equipment supports fabric inspection and garment quality control. Review product specifications and select equipment for your fabric type and testing requirements.

Conclusion

Accurate fabric GSM depends on representative sampling, a correct specimen area, reliable weighing, the right calculation and consistent testing conditions. If you are comparing a GSM Machine in Tirupur setup for your laboratory or production unit, review the GSM testing equipment from Amith Garment Services and match its specifications to your fabrics.

Frequently Asked Questions

1. How do you measure fabric GSM accurately?

Start with a representative fabric sample, free from creases, selvedge damage and distortion. Condition it as required by the applicable test method, then cut a specimen of known area, such as 100 cm² with a GSM round cutter. Weigh it on a calibrated balance, divide the weight in grams by the area in square metres, and compare the result with the specification. Repeat on several specimens from different positions and record the average, since one cut rarely represents a whole roll.

2. Which machine is used for fabric GSM testing?

Most laboratories use a GSM testing setup made of a GSM round cutter and a precision weighing balance. The cutter produces a specimen of fixed area, commonly 100 cm², and the balance records its weight. Some products sold as GSM testing machines bundle cutting and weighing, and others calculate GSM on a display. Because the term covers different configurations, check specimen area, balance readability and your fabric types before choosing. Amith Garment Services lists swatch and GSM cutting equipment on its website for review.

3. What is the difference between a GSM testing machine and a GSM calculator machine?

A GSM testing machine, or testing setup, prepares and weighs the specimen, usually through a cutter and a balance. A GSM calculator machine, or digital calculator, only performs the arithmetic once weight and area are known. It cannot cut a specimen or weigh it, so it cannot correct poor sampling or an uncalibrated balance. Laboratories needing specimen preparation, weighing and calculation in one workflow should confirm that the chosen product covers every step.

4. Where can I find a GSM Machine in Tirupur?

Textile testing equipment is usually sourced from specialist suppliers, so ask for specifications, calibration documents and support terms before ordering. Amith Garment Services is headquartered in Bangalore, and its website states that it supplies testing instruments across India, including Tirupur. This article does not confirm stock, pricing or a local branch, so contact the company directly through its website to check availability for your location.

5. What is a GSM machine used for?

A GSM machine helps determine fabric weight in grams per square metre. In practice, a cutter prepares a specimen of known area and a balance weighs it. Mills, garment exporters and testing labs use the result to check fabric against specifications.

6. How do I calculate the GSM of fabric at home or in a laboratory?

Cut a specimen of known area, weigh it in grams, and divide by the area in square metres. For a 100 cm² piece, multiply the weight in grams by 100. At home, results are only indicative without a calibrated balance.

7. Do I need a GSM cutter to measure fabric GSM?

Not strictly, but it helps. Any accurately measured specimen works, yet a GSM cutter gives a consistent area and clean edges, which improves repeatability. Hand-cut pieces can introduce area errors, especially on stretchy knits.

8. What should I check before buying a GSM testing machine?

Check specimen area, balance capacity and readability, calibration certificate, maintenance needs, available accessories, technical support and compatibility with your standard or buyer method. Ask for written specifications instead of relying on general descriptions.

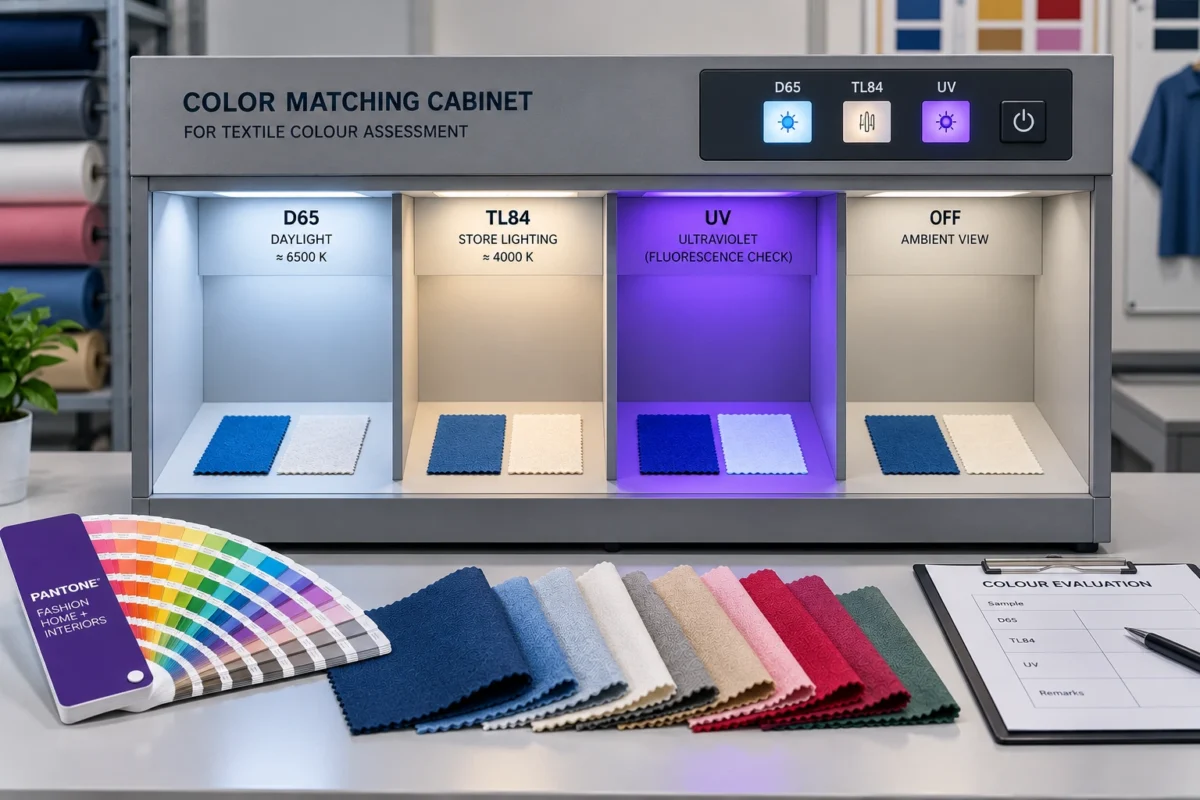
Color Matching Cabinet with D65, TL84 and UV light sources for textile colour assessment

D65, TL84 and UV Light Sources: What Is the Difference?

A fabric is approved in the lab, shipped to the buyer, and suddenly looks different under shop lighting. Anyone in garment manufacturing has seen this. A navy that looks right near a window can turn greyer under office tubes, and a white shirt can glow under UV in ways nobody expected. Often the cause is the light, not the fabric. That is why textile exporters, garment factories and testing laboratories across India, from Bangalore to Tiruppur, assess colour inside a Color Matching Cabinet, where illumination is controlled and repeatable.

What Is a Color Matching Cabinet?

Also called a colour matching light booth, it is an enclosed viewing cabinet fitted with standardised light sources and a neutral interior. It lets technicians compare fabric, trims and garments against an approved standard under controlled illumination instead of whatever room lighting happens to be available.

Room light changes with the time of day, window position and lamp age. Those shifts affect visual judgement. A colour matching cabinet fixes the lighting, and its neutral interior reduces the influence of surrounding colours.

It is a viewing tool, not a guarantee. Results still depend on the observer, the material and the procedure followed.

Why Are Different Light Sources Used for Colour Matching?

No single light represents every viewing condition. Textiles are seen in daylight, shops, offices and sometimes under UV, and colours can shift between them. Laboratories check samples under several light sources to catch differences that one illuminant alone would hide.

Every source spreads its energy across wavelengths differently. Fabric reflects that energy in its own way, so appearance changes with the light. This is the root of metamerism. Checking daylight simulation, retail lighting and UV illumination gives a fuller picture than any one source.

What Is D65 Light Source?

D65 is a CIE standard illuminant that represents average daylight, with a correlated colour temperature of about 6500 K. In textile colour assessment, a D65 light source simulates daylight so technicians can compare fabric and garment colour against approved standards under controlled conditions.

D65 is not identical to natural sunlight, which varies with hour, season and sky. It is a defined reference, and cabinet lamps approximate it as artificial daylight. How closely they match depends on the lamp and system, so check the manufacturer’s specifications.

Colour temperature also describes only the overall tone of the light. Two lamps can both be rated near 6500 K and still render the same fabric differently, because their spectral characteristics differ.

What Is TL84 Light Source?

TL84 is a commonly used reference for commercial store lighting, based on a narrow-band fluorescent lamp with a colour temperature near 4000 K. Buyers use TL84 lighting to see how fabrics and garments may look under typical retail conditions.

TL84 began as a commercial lamp designation, so it is not a CIE standard illuminant like D65. It is often compared with the CIE F11 fluorescent series. Exact specifications vary by lamp and cabinet, so treat 4000 K as approximate. If a buyer names TL84 in their requirements, confirm which lamp they mean.

What Is a UV Light Source?

UV illumination in a colour matching cabinet reveals fluorescence. It mainly shows whether fabrics contain optical brightening agents, which absorb ultraviolet radiation and emit visible blue light. That is why white and pastel fabrics can look different under UV-containing light.

Many white and pastel textiles are treated with optical brighteners. Under a source with UV content they glow, and without it they look duller. UV assessment is therefore a fluorescence check, not ordinary visible-light colour matching. Some D65 simulators include UV content and others do not, so know what your cabinet provides.

D65 vs TL84 vs UV Light Source

D65 simulates daylight at about 6500 K, while TL84 represents retail fluorescent lighting at about 4000 K. Colours look cooler under D65 and warmer under TL84. UV is different: it is not a viewing condition but a way to detect fluorescence.

Feature D65 TL84 UV
Main purpose Daylight assessment Retail-light assessment Fluorescence check
Typical application Shade approval Buyer store-light check Whites, pastels
Approx. colour temperature ~6500 K ~4000 K Not applicable
Represents Standard daylight illuminant Commercial store lighting Ultraviolet radiation
Useful for Matching to standards Spotting retail shifts Detecting brighteners
UV component Varies by cabinet Usually minimal Primary feature
Common textile use Colour approval Garment and buyer checks Optical brightener checks

Values are approximate and vary by lamp and system.

Why Metamerism Matters in Textile Colour Matching

Metamerism is when two samples appear to match under one light but differ under another. It happens because their spectral reflectance curves differ, even though they look alike under the first illuminant. In textiles, it often arises when different dye combinations are used.

Imagine a bulk fabric that matches its standard under D65 but shows a visible difference under TL84. That can mean a rejected shipment. Exporters, garment manufacturers, buying houses, quality teams and merchandisers all share that risk. Checking multiple illuminants helps flag potential metameric pairs early, and instrumental measurement can support the visual check.

How a Color Matching Cabinet Helps Textile Laboratories

In a textile laboratory, a Color Matching Cabinet gives technicians controlled lighting and a consistent place to compare fabric against standards. It suits garments and trims as well, and it allows evaluation under multiple illuminants. That supports quality-control decisions and reduces dependence on changing room light.

Visual assessment should always follow the relevant laboratory or customer procedure, including ISO and AATCC practices where they apply.

D65, TL84 and UV: Which Light Should You Use?

There is no single best light. The choice depends on customer requirements, product application, export market, retail environment, material, the colour standard, laboratory procedure and the presence of optical brighteners.

A shirt for a European retailer may need D65 and TL84 checks. White sportswear may also need a UV check. Always start with the buyer’s written requirements.

Industries That Use Color Matching Cabinets

Beyond textile manufacturing, garment manufacturing and dyeing and finishing, they are common in export houses, buying houses, fabric testing laboratories and home textiles. Fashion and apparel teams use them, and printing and packaging sometimes do too. In India, Tiruppur’s knitwear exporters and Bangalore’s garment manufacturers regularly work to buyer-specified lighting. Quality-control departments use the cabinet daily for colour evaluation and textile inspection.

How to Choose the Right Color Matching Cabinet

Consider these points before buying:

  • Light sources: which of D65, TL84 and UV you actually need
  • Number of illuminants: match it to buyer requirements
  • Light uniformity across the viewing area
  • Interior surface and viewing environment
  • Lamp replacement availability, and a timer or hour meter
  • Colour evaluation needs and available laboratory space
  • Manufacturer specifications: ask for lamp data
  • Calibration and maintenance expectations
  • Compliance with customer or laboratory procedures

Why Choose Amith Garment Services for Textile Testing Equipment?

Amith Garment Services supplies textile testing equipment for garment and fabric laboratories. The range includes the colour matching cabinet, crock meter for colour fastness testing, washing fastness tester, GSM cutter, fabric inspection machine, bursting strength tester and fabric rolling machine.

These instruments cover practical quality-control needs in garment manufacturing and textile laboratories. The team can discuss your testing requirements and help you select suitable equipment. Confirm specifications against your own procedures before purchase.

Conclusion

D65 simulates daylight, TL84 represents common store lighting, and UV reveals fluorescence from optical brighteners. Each shows a different side of colour appearance, which is why they are not interchangeable. Used with the right procedure, a Color Matching Cabinet gives textile teams consistent, controlled conditions for colour evaluation, though it works best alongside trained observers and, where needed, instrumental measurement.

Frequently Asked Questions

A Color Matching Cabinet is used to assess fabric, trim and garment colour under controlled, repeatable lighting. Technicians compare a production sample with an approved standard under sources such as D65, TL84 and sometimes UV, away from changing room light. This helps textile laboratories, garment factories and buying houses make more consistent visual decisions. It does not replace instrumental measurement, and results still depend on the observer, material and the relevant customer or laboratory procedure.

D65 is a CIE standard illuminant that represents average daylight at roughly 6500 K, so it is used to judge colour under daylight-like conditions. TL84 is a commercial fluorescent reference associated with store lighting, with a colour temperature near 4000 K. D65 shows how a colour behaves in daylight, while TL84 shows how it may look in a shop. Exact specifications vary by lamp and cabinet, so always check the manufacturer's data.

UV light is used to reveal fluorescence, mainly in fabrics treated with optical brightening agents. These agents absorb ultraviolet radiation and re-emit it as visible blue light, making whites and pastels look brighter. Checking under UV helps technicians see whether two samples contain different levels of brightener, which could cause a visible mismatch under certain lighting. It is a fluorescence check rather than a replacement for visible-light colour matching.

Yes. This is called metamerism. Two samples can have different spectral reflectance, such as when different dye combinations are used, yet look identical under one illuminant. Under another light with a different spectral distribution, such as TL84, the difference may become visible. That is why laboratories check important shades under more than one light source before approving a lot or shipping to a buyer.

It's a viewing cabinet with standard lights that lets you compare fabric colours under controlled lighting. Textile labs and garment factories use it to check a sample against an approved standard without room lighting changing the result.

D65 is a standard daylight reference at about 6500 Kelvin. In a colour matching cabinet, it simulates daylight so you can judge how a fabric colour compares with its approved standard.

TL84 is a commonly used store-lighting reference at around 4000 Kelvin. Buyers and garment makers use it to see how a fabric or garment colour will look under typical shop lighting.

They use UV light to spot fluorescence, especially from optical brighteners in white and pastel fabrics. It shows whether a fabric glows under ultraviolet, which can change how it looks under some lighting.

Pantone Color Standards used for textile colour matching and quality control

What Are Pantone Color Standards and Why Are They Important?

What Are Pantone Color Standards?

Pantone Color Standards are the standardized colour references built around the Pantone Color System, where each shade carries its own identifier. A name like “sky blue” is open to interpretation. A code is not.

For textiles, designers typically cite codes from Pantone’s fashion and home range, often supplied as cotton-based swatches (TCX). Manufacturers then treat that code as the target during development, lab dipping and production.

Pantone Color Standards are standardized, coded colour references that let designers, buyers and manufacturers specify the same shade without relying on subjective names. Each colour has a unique identifier, which reduces misunderstandings during development, sampling and production, especially across suppliers and countries.

Why Are Pantone Color Standards Important in Textile Manufacturing?

Colour is usually the first thing a buyer notices and the first reason a shipment is questioned. A shared reference helps at every stage: fabric development, sampling, dyeing, printing, bulk production, buyer approvals and export documentation.

Picture a knitwear order. The buyer sends a code, the mill dyes a lab dip, and the garment factory cuts panels from two dye lots. Without a common reference, each party judges “close enough” differently. With one, the disagreement becomes a discussion about measurable deviation rather than opinion.

Why are they important? They give everyone in the supply chain the same colour target. That reduces sampling rounds, limits shade disputes, supports buyer approvals and makes quality control more objective across fabric, printing and garment production.

How Do Pantone Color Standards Work?

The usual workflow looks like this:

  1. The buyer or designer selects a colour reference.
  2. The code is communicated to the manufacturer.
  3. Lab dips or fabric samples are prepared.
  4. Colour is evaluated under controlled lighting.
  5. Recipes are adjusted where necessary.
  6. The approved shade becomes the production reference.
  7. Bulk production is checked against that approved standard.

How are Pantone colours used in textiles? Designers cite a code in the tech pack, mills and dyeing units use it as the lab-dip target, and quality teams compare bulk fabric or garments against the approved shade under controlled light.

One caution: the same code will not look identical on every material. Fibre type, dye chemistry, fabric construction, finishing, surface texture, printing method and viewing conditions all shift appearance. A Pantone reference is a target, not a guarantee of an exact physical match on every substrate.

Pantone Color Standards vs Pantone Colour Guides

The two terms are often used interchangeably, but they play different roles. Broadly, the standards are the coded colour references. The guides are the tools that present them.

Factor Pantone Color Standards Pantone Colour Guides
Purpose Define and codify reference colours Present those colours as physical or digital swatches
Colour Reference The coded shade identity A printed or dyed representation of it
Manufacturing Use Target for development and approval Visual aid in the office, lab or floor
Textile Application Specifying fabrics, trims and garments Substrate-specific guides (e.g., cotton) for selection
Quality Control Basis for deviation checks Visual comparison only; sensitive to light and ageing
Buyer Communication Codes in tech packs and approvals Shows intent alongside the code

Pantone offers several systems and formats, and the Pantone Matching System (PMS) is best known in print. Always confirm which one your buyer specifies.

Why Is Pantone Colour Matching Important for Fabrics?

Pantone colour matching links design intent to real cloth. It shapes shade development, lab dips, dyeing, fabric inspection, buyer approval and shade consistency in bulk.

What is Pantone colour matching? It is the process of adjusting a dye or print recipe until a fabric sample aligns with a chosen Pantone reference within an agreed tolerance, usually checked under standardized lighting before buyer approval.

Ordinary office light or window daylight is a poor judge. Both change through the day and with the weather. Controlled lighting gives every evaluator the same conditions, so a disagreement reflects the fabric, not the room.

Role of a Color Matching Cabinet in Pantone Colour Evaluation

A Color Matching Cabinet, also called a light booth, provides standardized light sources inside a neutral enclosure. Common options include daylight simulation, TL84 store lighting, and incandescent or UV sources.

Why several? Metamerism. Two samples can match under one illuminant and visibly differ under another, often because different dyes were used. Checking under multiple sources exposes this before the buyer does. This textile laboratory equipment lets mills, factories and buyers compare shades under the same conditions.

What is the difference between Pantone and a colour matching cabinet? Pantone supplies the colour reference; the cabinet supplies the lighting to judge it. One defines the target, the other standardizes how you view the target and the sample.

Why is controlled lighting important? Colour appearance changes with the light source. Standardized illuminants and neutral surroundings let evaluators compare shades consistently and reveal metamerism, so decisions don’t depend on time of day, weather or room.

Pantone Color Standards and Textile Quality Control

Standardized references support quality control at each checkpoint:

  • Incoming fabric inspection: confirming supplied fabric against the reference
  • Lab dip approval: documenting the accepted shade
  • Production monitoring: catching drift between dye lots
  • Shade grouping: keeping panels from the same garment visually consistent
  • Final inspection and buyer approval: verifying against the signed-off standard

Colour consistency shapes perceived quality. A sleeve slightly off from the body panel reads as a defect, even when every strength test passes.

Factors That Can Affect Colour Matching

  • Fibre and construction: the same dye looks different on cotton, polyester or a textured knit.
  • Dye selection and concentration: small recipe changes shift the shade.
  • pH, temperature and processing time: a bath that runs slightly hotter or longer can change results.
  • Finishing: softeners and resin finishes may alter depth or tone.
  • Viewing conditions: lighting, viewing angle and surface gloss change perception.
  • Instrument calibration and sample preparation: uncalibrated devices or unevenly conditioned samples give misleading comparisons.

Pantone Color Standards in Garment Exporting

International buyers often specify colours by code, and Indian manufacturers, dyeing houses and fabric suppliers work from the same reference. In hubs such as Tiruppur, where knitwear exporters manage large repeat orders, and in Bangalore’s garment manufacturing sector, that shared reference helps keep shade expectations aligned across the textile industry. For textile exporters, a documented approved standard also makes it easier to resolve questions after shipment.

How to Maintain Better Colour Consistency in Textile Production

  • Use a defined colour reference for every order.
  • Keep approved lab-dip standards on file.
  • Evaluate shades under controlled lighting.
  • Hold dyeing and finishing parameters steady.
  • Calibrate relevant instruments.
  • Compare bulk production with the approved sample.
  • Record shade deviations and maintain testing documentation.
  • Train quality-control personnel.

Distinguish the two assessment methods. Visual assessment relies on trained observers under standard light. Instrumental measurement uses a spectrophotometer to quantify colour difference numerically. Most laboratories use both, and both are commonly guided by AATCC and ISO practices.

Choosing the Right Textile Colour Testing Equipment

Consider the application, testing requirements, lighting needs, compatibility with the standards your buyers use, and how the equipment fits your laboratory workflow. Then look at repeatability, calibration, ease of operation, maintenance, documentation and production volume. A small sampling unit and a large export facility may need very different textile testing equipment. Garment testing instruments for colour should sit alongside those for fastness and physical properties, not in isolation.

Why Choose Amith Garment Services?

Amith Garment Services provides textile testing equipment and related solutions for textile and garment quality-control applications. The range relevant to colour and fabric evaluation includes the Color Matching Cabinet, Crock Meter, Washing Fastness Tester, GSM Cutter, Fabric Inspection Machine, Bursting Strength Tester and Fabric Rolling Machine. Together, these help laboratories check colour, fastness and physical properties in one workflow. For advice on matching equipment to your testing requirements, contact the team through the website.

Conclusion

Pantone Color Standards turn subjective colour talk into a shared, documented reference that suits the realities of textile manufacturing. They work best when combined with lab dips, controlled lighting, calibrated instruments and disciplined records. Used that way, they help mills, factories and exporters deliver colour their buyers expect.

Frequently Asked Questions

Pantone Color Standards are used to specify, communicate and verify colour throughout textile production. Designers cite a code in the tech pack, mills and dyeing units use it as the target for lab dips, and quality teams compare bulk fabric or finished garments against the approved shade. Because the reference is coded rather than described in words, it cuts down on misinterpretation between buyers, factories and suppliers. It works best when paired with controlled lighting and, where required, instrumental colour measurement.

Pantone colour matching gives garment manufacturers a clear target from the first sample. Merchandisers can brief the dyeing unit with a code instead of a vague description, which can shorten lab-dip rounds and reduce shade disputes at approval. During production, the approved standard lets quality teams judge whether dye lots and panels stay within tolerance. It also supports smoother communication with international buyers, who often specify colours by code, though the final match still depends on the fabric and process.

Not always. A Pantone reference is a colour target, but fabrics respond differently to dyes and finishes. Fibre type, yarn and fabric construction, dye class, finishing and surface texture all influence how a shade appears, so a colour achieved on cotton may look different on polyester or a textured knit. Some colours may also fall outside what a given dye system can reproduce. Manufacturers therefore prepare lab dips, evaluate them under standardized light, and agree tolerances with the buyer rather than assuming an identical match.

A Color Matching Cabinet provides standardized, repeatable lighting so shade comparisons don't depend on the time of day, weather or room. Most offer several light sources, such as daylight, store lighting, and incandescent or UV, which helps reveal metamerism, where samples match under one light but not another. Using the same conditions at the mill, the factory and the buyer's office makes Pantone Color Standards easier to apply consistently. It supports visual assessment but does not replace instrumental measurement when numerical data is required.

They define and communicate colour with a code instead of a description. In textiles, buyers and manufacturers use them to agree on a shade, prepare lab dips, and check bulk production against the approved colour.

First, the buyer picks a Pantone code. The mill prepares lab dips to match it, and the shade is checked under controlled lighting. Once approved, that sample becomes the production standard, and bulk fabric is compared against it.

Because a code means the same thing to everyone. Instead of arguing over what "olive green" means, buyers, dyeing units and garment factories work from one reference, which cuts down on shade misunderstandings and rework.

Place the fabric and the approved standard side by side in a colour matching cabinet, then view them under standard light sources such as daylight. If needed, confirm with a spectrophotometer to measure the colour difference numerically.

Fabric inspection machine with fabric roll passing over illuminated inspection surface

What Is a Fabric Inspection Machine?

Every garment starts with fabric, and every fabric roll carries some risk. One hidden flaw can ruin dozens of cut panels. That is why a fabric inspection machine sits at the centre of fabric quality control in mills, garment factories and buying-house labs across India, from Tiruppur to Bangalore.

This guide explains what the equipment does, how inspection works, which defects matter, and how to choose the right setup.

What Is a Fabric Inspection Machine?

A fabric inspection machine is textile equipment that moves a fabric roll across an illuminated inspection surface so operators can spot, measure and record defects such as holes, stains, slubs and shade variation. It lets quality teams check fabric before cutting, stitching or finishing.

You may also hear it called a textile inspection machine, fabric roll inspection machine or fabric quality checking machine. A simple fabric inspection table serves the same purpose on a smaller scale.

Most machines are operator-assisted. The machine feeds, rewinds and measures the fabric, while a trained inspector judges what is a defect. Camera-based fabric defect detection systems also exist, but they are a separate category.

Why Is a Fabric Inspection Machine Important?

Fabric inspection matters because defects found before cutting cost far less than defects found in finished garments. It helps mills, exporters and buying houses grade fabric consistently, meet buyer specifications, and reduce avoidable rework, rejections and disputes over fabric quality.

Think of a garment exporter in Tiruppur who cuts 5,000 pieces from a lot with an unnoticed shade band. The problem surfaces only after stitching, and by then the fabric has been consumed. Textile quality control at the fabric stage prevents that.

Fabric manufacturers and textile mills also use inspection before dispatch. Documented results give both sides a shared reference if a claim arises.

How Does a Fabric Inspection Machine Work?

Operators load the roll, pass fabric over a lit inspection surface at a controlled speed, watch for flaws, and mark each one while the machine measures length. The roll is rewound with defect locations noted, so the team can grade it against a chosen standard.

The fabric moves through the machine under light tension. When the inspector sees a defect, they stop the roll, record its type and position, and often tag the selvage or the fabric itself.

Four factors decide how much you actually see:

  • Lighting: poor or uneven light hides faults, especially in dark or pale shades.
  • Tension: too tight and the fabric stretches, too loose and it wrinkles.
  • Speed: fast running lets defects slip past.
  • Operator training: consistent judgement matters as much as the equipment.

Key Features of a Fabric Inspection Machine

Configuration varies by model and application. No single machine has every item below, but these are the parts you will commonly find:

  • Inspection table or surface with a tilted or vertical viewing area
  • Fabric roll holder and spreading or feeding mechanism
  • Lighting system matched to the fabric and buyer requirements
  • Speed control for the fabric
  • Fabric tension control to keep the surface flat
  • Length measurement system for metre or yard counting
  • Defect marking and operator controls
  • Roll winding mechanism to rewind after inspection

Types of Fabric Defects Detected During Inspection

Inspection can reveal holes, stains, slubs, missing yarns, colour variation, bowing, skewing, creases, needle lines, oil marks, and printing, dyeing or selvage faults. Visibility depends on lighting, tension, speed and inspector training, since most machines assist the operator rather than detect automatically.

Fabric Defect What It Means Possible Cause Why It Matters
Hole Open break in the fabric Broken yarns, sharp objects, mishandling Panel becomes unusable
Stain / oil mark Foreign mark on the surface Machine oil, handling, storage May not wash out; visible on garment
Slub Thick, uneven yarn section Yarn spinning irregularity Affects appearance and hand feel
Missing yarn Gap in warp or weft Yarn breakage during weaving Creates lines or weak areas
Colour variation Shade difference within or between rolls Dyeing inconsistency Mismatched garment parts
Bowing Curved weft lines Uneven stress in finishing Distorted patterns and seams
Skewing Angled weft or course lines Finishing or handling issues Twisting in finished garments
Crease Permanent fold marks Poor rolling or storage Hard to remove; visible flaws
Needle line Vertical line in knits Damaged needle in knitting machine Repeats along the roll length
Selvage defect Uneven or damaged edge Weaving or finishing faults Reduces usable fabric width
Print / dyeing defect Misregistration, patches, streaks Process control problems Affects appearance and acceptance

Fabric Inspection Process Step by Step

  1. Record roll details: lot, roll number, width, stated length.
  2. Check the environment: lighting and cleanliness of the surface.
  3. Mount the roll and thread fabric with correct tension.
  4. Set inspection speed suited to the fabric.
  5. Inspect and mark defects as the fabric passes.
  6. Measure length and width during the run.
  7. Grade and record results for each roll, then rewind.

Fabric roll inspection is the examination of an entire roll, metre by metre, to find defects, measure length and assign a quality grade. It is usually done before cutting, and results are recorded per roll so lots can be accepted, rejected or negotiated.

Fabric Inspection Standards and Quality Control

Many buyers grade fabric using a point system. ASTM D5430 covers visual inspection and grading of fabrics, and the four-point system is widely used in the garment trade. Some buyers specify their own or other systems, and ISO and ASTM textile testing standards may apply to related tests.

The right procedure depends on fabric type, buyer requirements, end use and applicable quality specifications. No single standard fits every fabric or every inspection system. Always confirm what your buyer requires.

Industries That Use Fabric Inspection Machines

Fabric inspection is common across the textile value chain:

  • Textile mills and fabric manufacturers
  • Garment factories and garment exporters
  • Buying houses and third-party inspection teams
  • Fabric testing labs
  • Processing units before printing, dyeing or finishing
  • Importers checking incoming lots

Factors to Consider When Choosing a Fabric Inspection Machine

Consider fabric width and roll diameter, lighting quality, speed control, tension handling, length measurement, defect marking, build quality, operator comfort, after-sales support and total cost. Match the specification to your fabric types and buyer inspection requirements rather than to price alone.

Ask a fabric inspection machine manufacturer about roll capacity, whether the unit handles woven and knitted fabric, and what calibration and service support is available.

Fabric inspection machine price varies with size, features, measurement systems and build. Compare specifications and support, not just the quoted figure.

How a Fabric Inspection Machine Improves Textile Quality

Inspection improves garment quality by keeping flawed fabric out of cutting and sewing. Teams can mark, cut around or reject defective sections, segregate lots by shade, and give suppliers documented feedback, so fewer faults reach stitched garments.

It does not make fabric defect-free. It gives you information early, when you can still act on it. Combined with other fabric testing equipment such as GSM, colour and strength testers, it supports complete garment quality testing.

Fabric Inspection Machine vs Manual Fabric Inspection

Manual inspection relies on a table or hand-held fabric with more handling and less measurement. A machine feeds and rewinds the roll under controlled lighting and speed, adding length measurement and easier record keeping. Machines suit routine production checks; simple tables suit small samples.

Parameter Manual Inspection Fabric Inspection Machine
Inspection speed Depends on operator, often slower More controlled and steady
Operator effort Higher physical handling Lower; feeding assisted
Fabric handling More manual pulling Guided feeding and rewinding
Defect visibility Varies with room lighting Dedicated lighting on surface
Measurement Manual tape or estimate Built-in length measurement (model dependent)
Record keeping Handwritten Easier to standardise
Consistency Varies between operators Better process consistency
Production suitability Samples, small lots Routine roll inspection
QC applications Spot checks Full roll grading

Why Choose Amith Garment Services

Amith Garment Services supplies textile testing equipment and garment testing instruments for mills, labs and exporters. Fabric inspection is one part of a wider quality-control setup, so you can pair it with tools such as a crock meter, light booth or GSM cutter under one roof.

Talk through your fabric types, roll sizes and buyer requirements, and choose equipment that fits your actual workflow.

Conclusion

A fabric inspection machine gives textile and garment businesses a reliable way to find fabric problems before they become expensive. It cannot guarantee flawless fabric, but with proper lighting, tension, speed and trained inspectors, it makes fabric quality inspection more consistent and better documented.

Choose based on your fabric, buyer standards and workflow, and treat inspection as one step in a wider textile quality control system.

```html

Frequently Asked Questions

A fabric inspection machine is textile equipment that passes fabric rolls over an illuminated surface so trained operators can identify, mark and record defects. Depending on the model, it also measures fabric length and rewinds the roll after checking. Mills, garment exporters and quality labs use it to assess fabric before cutting, stitching, printing or finishing.

Fabric defects that go unnoticed become garment defects. Finding a hole, stain or shade variation before cutting lets teams mark, avoid or reject the affected section instead of wasting cutting, stitching and finishing effort. Inspection also gives exporters and buying houses documented evidence to support fabric acceptance decisions and conversations with suppliers.

A fabric inspection machine helps operators see holes, stains, oil marks, slubs, missing yarns, colour variation, bowing, skewing, creases, needle lines, and printing, dyeing or selvage defects. Most machines are operator-assisted, so what gets identified depends on lighting, fabric tension, running speed and the inspector's training and experience.

Start with your fabric: type, width, roll diameter and whether it is woven or knitted. Then compare lighting, speed control, tension handling, length measurement, defect marking and build quality. Check your buyer's inspection requirements, ask the manufacturer about service and calibration support, and consider total cost rather than price alone.

It's used to check fabric rolls for defects like holes, stains and colour differences before cutting. It also measures length and helps teams record and grade fabric quality.

It moves the fabric over a lit surface at a steady speed. An operator watches for flaws, marks them, and the machine measures length while rewinding the roll.

It finds problems early, before the fabric is cut. That helps you avoid wasted material, sort fabric by quality, and share clear records with suppliers and buyers.

Common ones include holes, stains, slubs, missing yarns, shade variation, bowing, skewing, creases, needle lines, and printing or dyeing faults.

```