What Are Pantone Color Standards?
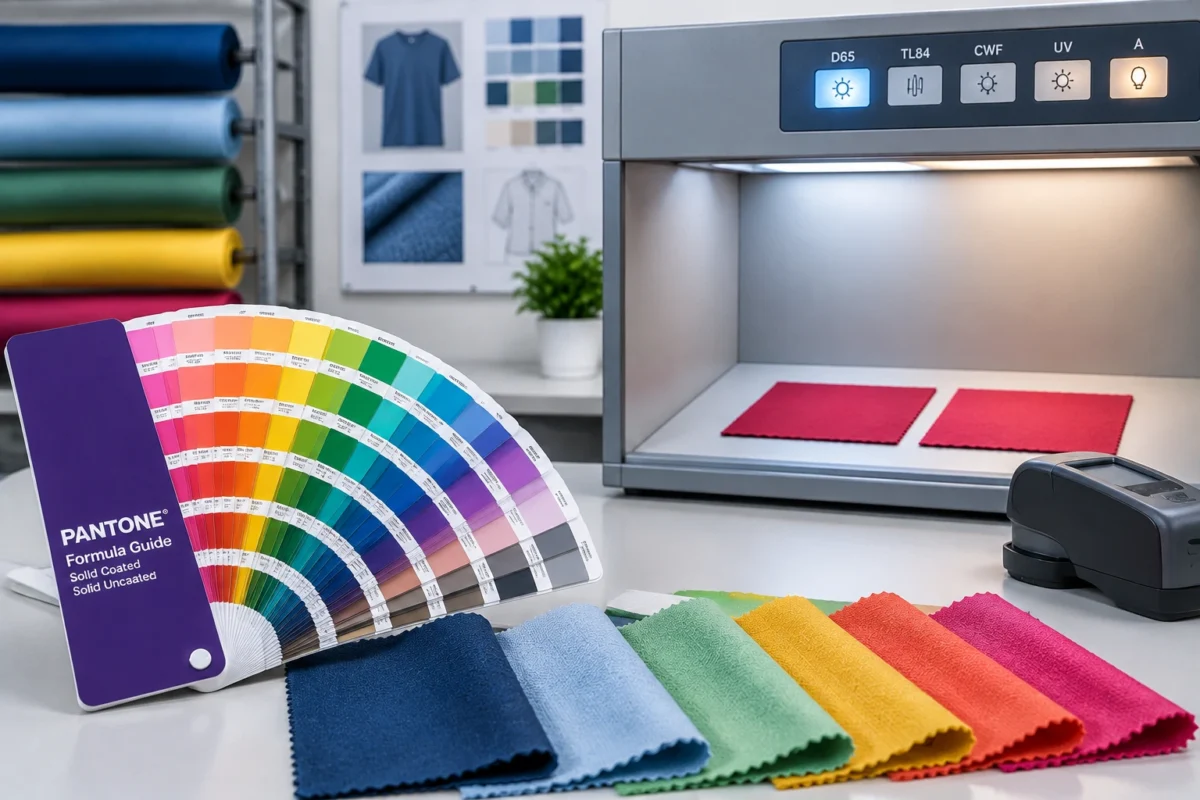
Pantone Color Standards are the standardized colour references built around the Pantone Color System, where each shade carries its own identifier. A name like “sky blue” is open to interpretation. A code is not.
For textiles, designers typically cite codes from Pantone’s fashion and home range, often supplied as cotton-based swatches (TCX). Manufacturers then treat that code as the target during development, lab dipping and production.
Pantone Color Standards are standardized, coded colour references that let designers, buyers and manufacturers specify the same shade without relying on subjective names. Each colour has a unique identifier, which reduces misunderstandings during development, sampling and production, especially across suppliers and countries.
Why Are Pantone Color Standards Important in Textile Manufacturing?
Colour is usually the first thing a buyer notices and the first reason a shipment is questioned. A shared reference helps at every stage: fabric development, sampling, dyeing, printing, bulk production, buyer approvals and export documentation.
Picture a knitwear order. The buyer sends a code, the mill dyes a lab dip, and the garment factory cuts panels from two dye lots. Without a common reference, each party judges “close enough” differently. With one, the disagreement becomes a discussion about measurable deviation rather than opinion.
Why are they important? They give everyone in the supply chain the same colour target. That reduces sampling rounds, limits shade disputes, supports buyer approvals and makes quality control more objective across fabric, printing and garment production.
How Do Pantone Color Standards Work?
The usual workflow looks like this:
- The buyer or designer selects a colour reference.
- The code is communicated to the manufacturer.
- Lab dips or fabric samples are prepared.
- Colour is evaluated under controlled lighting.
- Recipes are adjusted where necessary.
- The approved shade becomes the production reference.
- Bulk production is checked against that approved standard.
How are Pantone colours used in textiles? Designers cite a code in the tech pack, mills and dyeing units use it as the lab-dip target, and quality teams compare bulk fabric or garments against the approved shade under controlled light.
One caution: the same code will not look identical on every material. Fibre type, dye chemistry, fabric construction, finishing, surface texture, printing method and viewing conditions all shift appearance. A Pantone reference is a target, not a guarantee of an exact physical match on every substrate.
Pantone Color Standards vs Pantone Colour Guides
The two terms are often used interchangeably, but they play different roles. Broadly, the standards are the coded colour references. The guides are the tools that present them.
| Factor | Pantone Color Standards | Pantone Colour Guides |
| Purpose | Define and codify reference colours | Present those colours as physical or digital swatches |
| Colour Reference | The coded shade identity | A printed or dyed representation of it |
| Manufacturing Use | Target for development and approval | Visual aid in the office, lab or floor |
| Textile Application | Specifying fabrics, trims and garments | Substrate-specific guides (e.g., cotton) for selection |
| Quality Control | Basis for deviation checks | Visual comparison only; sensitive to light and ageing |
| Buyer Communication | Codes in tech packs and approvals | Shows intent alongside the code |
Pantone offers several systems and formats, and the Pantone Matching System (PMS) is best known in print. Always confirm which one your buyer specifies.
Why Is Pantone Colour Matching Important for Fabrics?
Pantone colour matching links design intent to real cloth. It shapes shade development, lab dips, dyeing, fabric inspection, buyer approval and shade consistency in bulk.
What is Pantone colour matching? It is the process of adjusting a dye or print recipe until a fabric sample aligns with a chosen Pantone reference within an agreed tolerance, usually checked under standardized lighting before buyer approval.
Ordinary office light or window daylight is a poor judge. Both change through the day and with the weather. Controlled lighting gives every evaluator the same conditions, so a disagreement reflects the fabric, not the room.
Role of a Color Matching Cabinet in Pantone Colour Evaluation
A Color Matching Cabinet, also called a light booth, provides standardized light sources inside a neutral enclosure. Common options include daylight simulation, TL84 store lighting, and incandescent or UV sources.
Why several? Metamerism. Two samples can match under one illuminant and visibly differ under another, often because different dyes were used. Checking under multiple sources exposes this before the buyer does. This textile laboratory equipment lets mills, factories and buyers compare shades under the same conditions.
What is the difference between Pantone and a colour matching cabinet? Pantone supplies the colour reference; the cabinet supplies the lighting to judge it. One defines the target, the other standardizes how you view the target and the sample.
Why is controlled lighting important? Colour appearance changes with the light source. Standardized illuminants and neutral surroundings let evaluators compare shades consistently and reveal metamerism, so decisions don’t depend on time of day, weather or room.
Pantone Color Standards and Textile Quality Control
Standardized references support quality control at each checkpoint:
- Incoming fabric inspection: confirming supplied fabric against the reference
- Lab dip approval: documenting the accepted shade
- Production monitoring: catching drift between dye lots
- Shade grouping: keeping panels from the same garment visually consistent
- Final inspection and buyer approval: verifying against the signed-off standard
Colour consistency shapes perceived quality. A sleeve slightly off from the body panel reads as a defect, even when every strength test passes.
Factors That Can Affect Colour Matching
- Fibre and construction: the same dye looks different on cotton, polyester or a textured knit.
- Dye selection and concentration: small recipe changes shift the shade.
- pH, temperature and processing time: a bath that runs slightly hotter or longer can change results.
- Finishing: softeners and resin finishes may alter depth or tone.
- Viewing conditions: lighting, viewing angle and surface gloss change perception.
- Instrument calibration and sample preparation: uncalibrated devices or unevenly conditioned samples give misleading comparisons.
Pantone Color Standards in Garment Exporting
International buyers often specify colours by code, and Indian manufacturers, dyeing houses and fabric suppliers work from the same reference. In hubs such as Tiruppur, where knitwear exporters manage large repeat orders, and in Bangalore’s garment manufacturing sector, that shared reference helps keep shade expectations aligned across the textile industry. For textile exporters, a documented approved standard also makes it easier to resolve questions after shipment.
How to Maintain Better Colour Consistency in Textile Production
- Use a defined colour reference for every order.
- Keep approved lab-dip standards on file.
- Evaluate shades under controlled lighting.
- Hold dyeing and finishing parameters steady.
- Calibrate relevant instruments.
- Compare bulk production with the approved sample.
- Record shade deviations and maintain testing documentation.
- Train quality-control personnel.
Distinguish the two assessment methods. Visual assessment relies on trained observers under standard light. Instrumental measurement uses a spectrophotometer to quantify colour difference numerically. Most laboratories use both, and both are commonly guided by AATCC and ISO practices.
Choosing the Right Textile Colour Testing Equipment
Consider the application, testing requirements, lighting needs, compatibility with the standards your buyers use, and how the equipment fits your laboratory workflow. Then look at repeatability, calibration, ease of operation, maintenance, documentation and production volume. A small sampling unit and a large export facility may need very different textile testing equipment. Garment testing instruments for colour should sit alongside those for fastness and physical properties, not in isolation.
Why Choose Amith Garment Services?
Amith Garment Services provides textile testing equipment and related solutions for textile and garment quality-control applications. The range relevant to colour and fabric evaluation includes the Color Matching Cabinet, Crock Meter, Washing Fastness Tester, GSM Cutter, Fabric Inspection Machine, Bursting Strength Tester and Fabric Rolling Machine. Together, these help laboratories check colour, fastness and physical properties in one workflow. For advice on matching equipment to your testing requirements, contact the team through the website.
Conclusion
Pantone Color Standards turn subjective colour talk into a shared, documented reference that suits the realities of textile manufacturing. They work best when combined with lab dips, controlled lighting, calibrated instruments and disciplined records. Used that way, they help mills, factories and exporters deliver colour their buyers expect.
Frequently Asked Questions
Pantone Color Standards are used to specify, communicate and verify colour throughout textile production. Designers cite a code in the tech pack, mills and dyeing units use it as the target for lab dips, and quality teams compare bulk fabric or finished garments against the approved shade. Because the reference is coded rather than described in words, it cuts down on misinterpretation between buyers, factories and suppliers. It works best when paired with controlled lighting and, where required, instrumental colour measurement.
Pantone colour matching gives garment manufacturers a clear target from the first sample. Merchandisers can brief the dyeing unit with a code instead of a vague description, which can shorten lab-dip rounds and reduce shade disputes at approval. During production, the approved standard lets quality teams judge whether dye lots and panels stay within tolerance. It also supports smoother communication with international buyers, who often specify colours by code, though the final match still depends on the fabric and process.
Not always. A Pantone reference is a colour target, but fabrics respond differently to dyes and finishes. Fibre type, yarn and fabric construction, dye class, finishing and surface texture all influence how a shade appears, so a colour achieved on cotton may look different on polyester or a textured knit. Some colours may also fall outside what a given dye system can reproduce. Manufacturers therefore prepare lab dips, evaluate them under standardized light, and agree tolerances with the buyer rather than assuming an identical match.
A Color Matching Cabinet provides standardized, repeatable lighting so shade comparisons don't depend on the time of day, weather or room. Most offer several light sources, such as daylight, store lighting, and incandescent or UV, which helps reveal metamerism, where samples match under one light but not another. Using the same conditions at the mill, the factory and the buyer's office makes Pantone Color Standards easier to apply consistently. It supports visual assessment but does not replace instrumental measurement when numerical data is required.
They define and communicate colour with a code instead of a description. In textiles, buyers and manufacturers use them to agree on a shade, prepare lab dips, and check bulk production against the approved colour.
First, the buyer picks a Pantone code. The mill prepares lab dips to match it, and the shade is checked under controlled lighting. Once approved, that sample becomes the production standard, and bulk fabric is compared against it.
Because a code means the same thing to everyone. Instead of arguing over what "olive green" means, buyers, dyeing units and garment factories work from one reference, which cuts down on shade misunderstandings and rework.
Place the fabric and the approved standard side by side in a colour matching cabinet, then view them under standard light sources such as daylight. If needed, confirm with a spectrophotometer to measure the colour difference numerically.