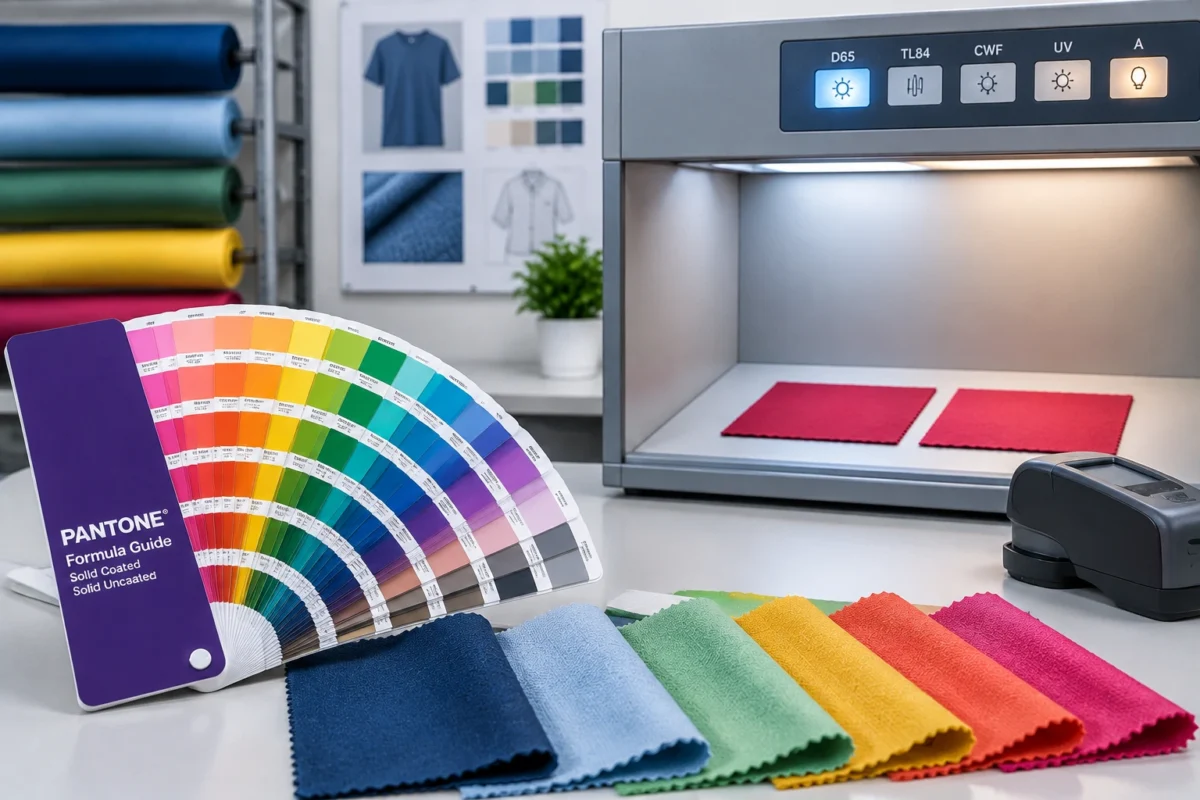
Pantone Color Standards used for textile colour matching and quality control

What Are Pantone Color Standards and Why Are They Important?

What Are Pantone Color Standards?

Pantone Color Standards are the standardized colour references built around the Pantone Color System, where each shade carries its own identifier. A name like “sky blue” is open to interpretation. A code is not.

For textiles, designers typically cite codes from Pantone’s fashion and home range, often supplied as cotton-based swatches (TCX). Manufacturers then treat that code as the target during development, lab dipping and production.

Pantone Color Standards are standardized, coded colour references that let designers, buyers and manufacturers specify the same shade without relying on subjective names. Each colour has a unique identifier, which reduces misunderstandings during development, sampling and production, especially across suppliers and countries.

Why Are Pantone Color Standards Important in Textile Manufacturing?

Colour is usually the first thing a buyer notices and the first reason a shipment is questioned. A shared reference helps at every stage: fabric development, sampling, dyeing, printing, bulk production, buyer approvals and export documentation.

Picture a knitwear order. The buyer sends a code, the mill dyes a lab dip, and the garment factory cuts panels from two dye lots. Without a common reference, each party judges “close enough” differently. With one, the disagreement becomes a discussion about measurable deviation rather than opinion.

Why are they important? They give everyone in the supply chain the same colour target. That reduces sampling rounds, limits shade disputes, supports buyer approvals and makes quality control more objective across fabric, printing and garment production.

How Do Pantone Color Standards Work?

The usual workflow looks like this:

  1. The buyer or designer selects a colour reference.
  2. The code is communicated to the manufacturer.
  3. Lab dips or fabric samples are prepared.
  4. Colour is evaluated under controlled lighting.
  5. Recipes are adjusted where necessary.
  6. The approved shade becomes the production reference.
  7. Bulk production is checked against that approved standard.

How are Pantone colours used in textiles? Designers cite a code in the tech pack, mills and dyeing units use it as the lab-dip target, and quality teams compare bulk fabric or garments against the approved shade under controlled light.

One caution: the same code will not look identical on every material. Fibre type, dye chemistry, fabric construction, finishing, surface texture, printing method and viewing conditions all shift appearance. A Pantone reference is a target, not a guarantee of an exact physical match on every substrate.

Pantone Color Standards vs Pantone Colour Guides

The two terms are often used interchangeably, but they play different roles. Broadly, the standards are the coded colour references. The guides are the tools that present them.

Factor Pantone Color Standards Pantone Colour Guides
Purpose Define and codify reference colours Present those colours as physical or digital swatches
Colour Reference The coded shade identity A printed or dyed representation of it
Manufacturing Use Target for development and approval Visual aid in the office, lab or floor
Textile Application Specifying fabrics, trims and garments Substrate-specific guides (e.g., cotton) for selection
Quality Control Basis for deviation checks Visual comparison only; sensitive to light and ageing
Buyer Communication Codes in tech packs and approvals Shows intent alongside the code

Pantone offers several systems and formats, and the Pantone Matching System (PMS) is best known in print. Always confirm which one your buyer specifies.

Why Is Pantone Colour Matching Important for Fabrics?

Pantone colour matching links design intent to real cloth. It shapes shade development, lab dips, dyeing, fabric inspection, buyer approval and shade consistency in bulk.

What is Pantone colour matching? It is the process of adjusting a dye or print recipe until a fabric sample aligns with a chosen Pantone reference within an agreed tolerance, usually checked under standardized lighting before buyer approval.

Ordinary office light or window daylight is a poor judge. Both change through the day and with the weather. Controlled lighting gives every evaluator the same conditions, so a disagreement reflects the fabric, not the room.

Role of a Color Matching Cabinet in Pantone Colour Evaluation

A Color Matching Cabinet, also called a light booth, provides standardized light sources inside a neutral enclosure. Common options include daylight simulation, TL84 store lighting, and incandescent or UV sources.

Why several? Metamerism. Two samples can match under one illuminant and visibly differ under another, often because different dyes were used. Checking under multiple sources exposes this before the buyer does. This textile laboratory equipment lets mills, factories and buyers compare shades under the same conditions.

What is the difference between Pantone and a colour matching cabinet? Pantone supplies the colour reference; the cabinet supplies the lighting to judge it. One defines the target, the other standardizes how you view the target and the sample.

Why is controlled lighting important? Colour appearance changes with the light source. Standardized illuminants and neutral surroundings let evaluators compare shades consistently and reveal metamerism, so decisions don’t depend on time of day, weather or room.

Pantone Color Standards and Textile Quality Control

Standardized references support quality control at each checkpoint:

  • Incoming fabric inspection: confirming supplied fabric against the reference
  • Lab dip approval: documenting the accepted shade
  • Production monitoring: catching drift between dye lots
  • Shade grouping: keeping panels from the same garment visually consistent
  • Final inspection and buyer approval: verifying against the signed-off standard

Colour consistency shapes perceived quality. A sleeve slightly off from the body panel reads as a defect, even when every strength test passes.

Factors That Can Affect Colour Matching

  • Fibre and construction: the same dye looks different on cotton, polyester or a textured knit.
  • Dye selection and concentration: small recipe changes shift the shade.
  • pH, temperature and processing time: a bath that runs slightly hotter or longer can change results.
  • Finishing: softeners and resin finishes may alter depth or tone.
  • Viewing conditions: lighting, viewing angle and surface gloss change perception.
  • Instrument calibration and sample preparation: uncalibrated devices or unevenly conditioned samples give misleading comparisons.

Pantone Color Standards in Garment Exporting

International buyers often specify colours by code, and Indian manufacturers, dyeing houses and fabric suppliers work from the same reference. In hubs such as Tiruppur, where knitwear exporters manage large repeat orders, and in Bangalore’s garment manufacturing sector, that shared reference helps keep shade expectations aligned across the textile industry. For textile exporters, a documented approved standard also makes it easier to resolve questions after shipment.

How to Maintain Better Colour Consistency in Textile Production

  • Use a defined colour reference for every order.
  • Keep approved lab-dip standards on file.
  • Evaluate shades under controlled lighting.
  • Hold dyeing and finishing parameters steady.
  • Calibrate relevant instruments.
  • Compare bulk production with the approved sample.
  • Record shade deviations and maintain testing documentation.
  • Train quality-control personnel.

Distinguish the two assessment methods. Visual assessment relies on trained observers under standard light. Instrumental measurement uses a spectrophotometer to quantify colour difference numerically. Most laboratories use both, and both are commonly guided by AATCC and ISO practices.

Choosing the Right Textile Colour Testing Equipment

Consider the application, testing requirements, lighting needs, compatibility with the standards your buyers use, and how the equipment fits your laboratory workflow. Then look at repeatability, calibration, ease of operation, maintenance, documentation and production volume. A small sampling unit and a large export facility may need very different textile testing equipment. Garment testing instruments for colour should sit alongside those for fastness and physical properties, not in isolation.

Why Choose Amith Garment Services?

Amith Garment Services provides textile testing equipment and related solutions for textile and garment quality-control applications. The range relevant to colour and fabric evaluation includes the Color Matching Cabinet, Crock Meter, Washing Fastness Tester, GSM Cutter, Fabric Inspection Machine, Bursting Strength Tester and Fabric Rolling Machine. Together, these help laboratories check colour, fastness and physical properties in one workflow. For advice on matching equipment to your testing requirements, contact the team through the website.

Conclusion

Pantone Color Standards turn subjective colour talk into a shared, documented reference that suits the realities of textile manufacturing. They work best when combined with lab dips, controlled lighting, calibrated instruments and disciplined records. Used that way, they help mills, factories and exporters deliver colour their buyers expect.

Frequently Asked Questions

Pantone Color Standards are used to specify, communicate and verify colour throughout textile production. Designers cite a code in the tech pack, mills and dyeing units use it as the target for lab dips, and quality teams compare bulk fabric or finished garments against the approved shade. Because the reference is coded rather than described in words, it cuts down on misinterpretation between buyers, factories and suppliers. It works best when paired with controlled lighting and, where required, instrumental colour measurement.

Pantone colour matching gives garment manufacturers a clear target from the first sample. Merchandisers can brief the dyeing unit with a code instead of a vague description, which can shorten lab-dip rounds and reduce shade disputes at approval. During production, the approved standard lets quality teams judge whether dye lots and panels stay within tolerance. It also supports smoother communication with international buyers, who often specify colours by code, though the final match still depends on the fabric and process.

Not always. A Pantone reference is a colour target, but fabrics respond differently to dyes and finishes. Fibre type, yarn and fabric construction, dye class, finishing and surface texture all influence how a shade appears, so a colour achieved on cotton may look different on polyester or a textured knit. Some colours may also fall outside what a given dye system can reproduce. Manufacturers therefore prepare lab dips, evaluate them under standardized light, and agree tolerances with the buyer rather than assuming an identical match.

A Color Matching Cabinet provides standardized, repeatable lighting so shade comparisons don't depend on the time of day, weather or room. Most offer several light sources, such as daylight, store lighting, and incandescent or UV, which helps reveal metamerism, where samples match under one light but not another. Using the same conditions at the mill, the factory and the buyer's office makes Pantone Color Standards easier to apply consistently. It supports visual assessment but does not replace instrumental measurement when numerical data is required.

They define and communicate colour with a code instead of a description. In textiles, buyers and manufacturers use them to agree on a shade, prepare lab dips, and check bulk production against the approved colour.

First, the buyer picks a Pantone code. The mill prepares lab dips to match it, and the shade is checked under controlled lighting. Once approved, that sample becomes the production standard, and bulk fabric is compared against it.

Because a code means the same thing to everyone. Instead of arguing over what "olive green" means, buyers, dyeing units and garment factories work from one reference, which cuts down on shade misunderstandings and rework.

Place the fabric and the approved standard side by side in a colour matching cabinet, then view them under standard light sources such as daylight. If needed, confirm with a spectrophotometer to measure the colour difference numerically.
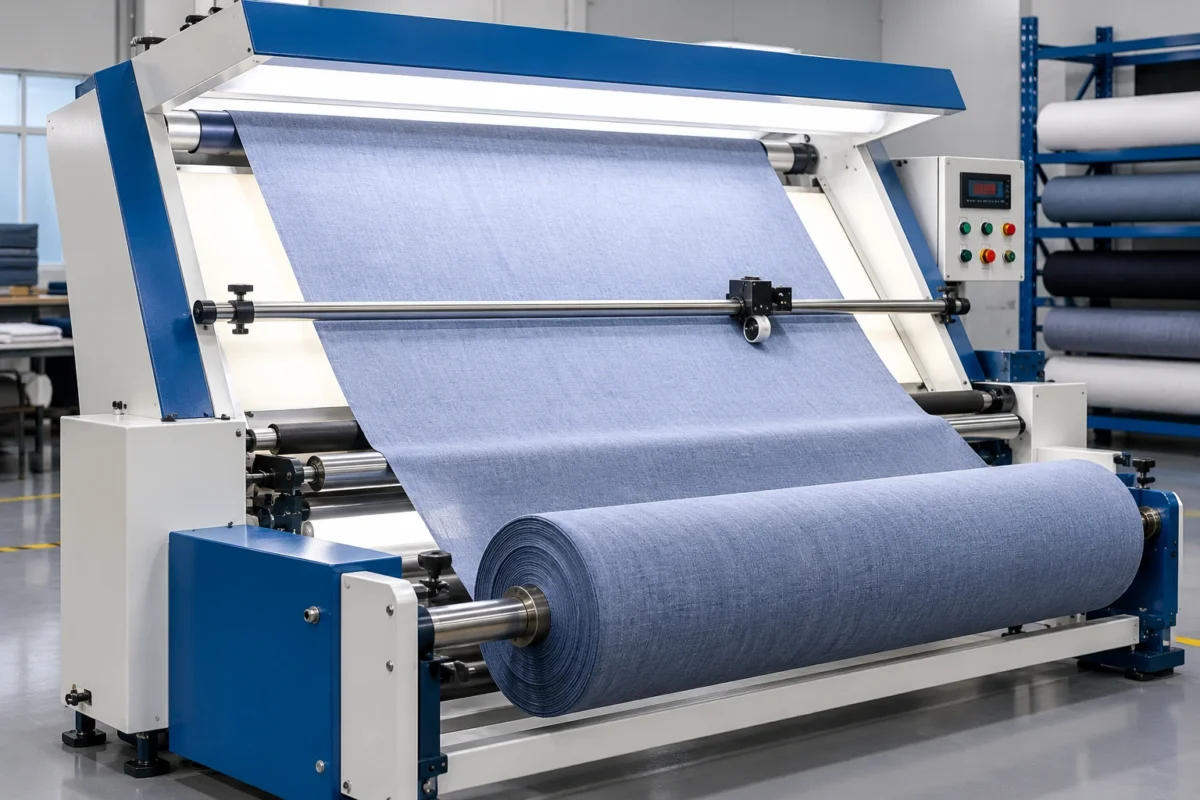
Fabric inspection machine with fabric roll passing over illuminated inspection surface

What Is a Fabric Inspection Machine?

Every garment starts with fabric, and every fabric roll carries some risk. One hidden flaw can ruin dozens of cut panels. That is why a fabric inspection machine sits at the centre of fabric quality control in mills, garment factories and buying-house labs across India, from Tiruppur to Bangalore.

This guide explains what the equipment does, how inspection works, which defects matter, and how to choose the right setup.

What Is a Fabric Inspection Machine?

A fabric inspection machine is textile equipment that moves a fabric roll across an illuminated inspection surface so operators can spot, measure and record defects such as holes, stains, slubs and shade variation. It lets quality teams check fabric before cutting, stitching or finishing.

You may also hear it called a textile inspection machine, fabric roll inspection machine or fabric quality checking machine. A simple fabric inspection table serves the same purpose on a smaller scale.

Most machines are operator-assisted. The machine feeds, rewinds and measures the fabric, while a trained inspector judges what is a defect. Camera-based fabric defect detection systems also exist, but they are a separate category.

Why Is a Fabric Inspection Machine Important?

Fabric inspection matters because defects found before cutting cost far less than defects found in finished garments. It helps mills, exporters and buying houses grade fabric consistently, meet buyer specifications, and reduce avoidable rework, rejections and disputes over fabric quality.

Think of a garment exporter in Tiruppur who cuts 5,000 pieces from a lot with an unnoticed shade band. The problem surfaces only after stitching, and by then the fabric has been consumed. Textile quality control at the fabric stage prevents that.

Fabric manufacturers and textile mills also use inspection before dispatch. Documented results give both sides a shared reference if a claim arises.

How Does a Fabric Inspection Machine Work?

Operators load the roll, pass fabric over a lit inspection surface at a controlled speed, watch for flaws, and mark each one while the machine measures length. The roll is rewound with defect locations noted, so the team can grade it against a chosen standard.

The fabric moves through the machine under light tension. When the inspector sees a defect, they stop the roll, record its type and position, and often tag the selvage or the fabric itself.

Four factors decide how much you actually see:

  • Lighting: poor or uneven light hides faults, especially in dark or pale shades.
  • Tension: too tight and the fabric stretches, too loose and it wrinkles.
  • Speed: fast running lets defects slip past.
  • Operator training: consistent judgement matters as much as the equipment.

Key Features of a Fabric Inspection Machine

Configuration varies by model and application. No single machine has every item below, but these are the parts you will commonly find:

  • Inspection table or surface with a tilted or vertical viewing area
  • Fabric roll holder and spreading or feeding mechanism
  • Lighting system matched to the fabric and buyer requirements
  • Speed control for the fabric
  • Fabric tension control to keep the surface flat
  • Length measurement system for metre or yard counting
  • Defect marking and operator controls
  • Roll winding mechanism to rewind after inspection

Types of Fabric Defects Detected During Inspection

Inspection can reveal holes, stains, slubs, missing yarns, colour variation, bowing, skewing, creases, needle lines, oil marks, and printing, dyeing or selvage faults. Visibility depends on lighting, tension, speed and inspector training, since most machines assist the operator rather than detect automatically.

Fabric Defect What It Means Possible Cause Why It Matters
Hole Open break in the fabric Broken yarns, sharp objects, mishandling Panel becomes unusable
Stain / oil mark Foreign mark on the surface Machine oil, handling, storage May not wash out; visible on garment
Slub Thick, uneven yarn section Yarn spinning irregularity Affects appearance and hand feel
Missing yarn Gap in warp or weft Yarn breakage during weaving Creates lines or weak areas
Colour variation Shade difference within or between rolls Dyeing inconsistency Mismatched garment parts
Bowing Curved weft lines Uneven stress in finishing Distorted patterns and seams
Skewing Angled weft or course lines Finishing or handling issues Twisting in finished garments
Crease Permanent fold marks Poor rolling or storage Hard to remove; visible flaws
Needle line Vertical line in knits Damaged needle in knitting machine Repeats along the roll length
Selvage defect Uneven or damaged edge Weaving or finishing faults Reduces usable fabric width
Print / dyeing defect Misregistration, patches, streaks Process control problems Affects appearance and acceptance

Fabric Inspection Process Step by Step

  1. Record roll details: lot, roll number, width, stated length.
  2. Check the environment: lighting and cleanliness of the surface.
  3. Mount the roll and thread fabric with correct tension.
  4. Set inspection speed suited to the fabric.
  5. Inspect and mark defects as the fabric passes.
  6. Measure length and width during the run.
  7. Grade and record results for each roll, then rewind.

Fabric roll inspection is the examination of an entire roll, metre by metre, to find defects, measure length and assign a quality grade. It is usually done before cutting, and results are recorded per roll so lots can be accepted, rejected or negotiated.

Fabric Inspection Standards and Quality Control

Many buyers grade fabric using a point system. ASTM D5430 covers visual inspection and grading of fabrics, and the four-point system is widely used in the garment trade. Some buyers specify their own or other systems, and ISO and ASTM textile testing standards may apply to related tests.

The right procedure depends on fabric type, buyer requirements, end use and applicable quality specifications. No single standard fits every fabric or every inspection system. Always confirm what your buyer requires.

Industries That Use Fabric Inspection Machines

Fabric inspection is common across the textile value chain:

  • Textile mills and fabric manufacturers
  • Garment factories and garment exporters
  • Buying houses and third-party inspection teams
  • Fabric testing labs
  • Processing units before printing, dyeing or finishing
  • Importers checking incoming lots

Factors to Consider When Choosing a Fabric Inspection Machine

Consider fabric width and roll diameter, lighting quality, speed control, tension handling, length measurement, defect marking, build quality, operator comfort, after-sales support and total cost. Match the specification to your fabric types and buyer inspection requirements rather than to price alone.

Ask a fabric inspection machine manufacturer about roll capacity, whether the unit handles woven and knitted fabric, and what calibration and service support is available.

Fabric inspection machine price varies with size, features, measurement systems and build. Compare specifications and support, not just the quoted figure.

How a Fabric Inspection Machine Improves Textile Quality

Inspection improves garment quality by keeping flawed fabric out of cutting and sewing. Teams can mark, cut around or reject defective sections, segregate lots by shade, and give suppliers documented feedback, so fewer faults reach stitched garments.

It does not make fabric defect-free. It gives you information early, when you can still act on it. Combined with other fabric testing equipment such as GSM, colour and strength testers, it supports complete garment quality testing.

Fabric Inspection Machine vs Manual Fabric Inspection

Manual inspection relies on a table or hand-held fabric with more handling and less measurement. A machine feeds and rewinds the roll under controlled lighting and speed, adding length measurement and easier record keeping. Machines suit routine production checks; simple tables suit small samples.

Parameter Manual Inspection Fabric Inspection Machine
Inspection speed Depends on operator, often slower More controlled and steady
Operator effort Higher physical handling Lower; feeding assisted
Fabric handling More manual pulling Guided feeding and rewinding
Defect visibility Varies with room lighting Dedicated lighting on surface
Measurement Manual tape or estimate Built-in length measurement (model dependent)
Record keeping Handwritten Easier to standardise
Consistency Varies between operators Better process consistency
Production suitability Samples, small lots Routine roll inspection
QC applications Spot checks Full roll grading

Why Choose Amith Garment Services

Amith Garment Services supplies textile testing equipment and garment testing instruments for mills, labs and exporters. Fabric inspection is one part of a wider quality-control setup, so you can pair it with tools such as a crock meter, light booth or GSM cutter under one roof.

Talk through your fabric types, roll sizes and buyer requirements, and choose equipment that fits your actual workflow.

Conclusion

A fabric inspection machine gives textile and garment businesses a reliable way to find fabric problems before they become expensive. It cannot guarantee flawless fabric, but with proper lighting, tension, speed and trained inspectors, it makes fabric quality inspection more consistent and better documented.

Choose based on your fabric, buyer standards and workflow, and treat inspection as one step in a wider textile quality control system.

```html

Frequently Asked Questions

A fabric inspection machine is textile equipment that passes fabric rolls over an illuminated surface so trained operators can identify, mark and record defects. Depending on the model, it also measures fabric length and rewinds the roll after checking. Mills, garment exporters and quality labs use it to assess fabric before cutting, stitching, printing or finishing.

Fabric defects that go unnoticed become garment defects. Finding a hole, stain or shade variation before cutting lets teams mark, avoid or reject the affected section instead of wasting cutting, stitching and finishing effort. Inspection also gives exporters and buying houses documented evidence to support fabric acceptance decisions and conversations with suppliers.

A fabric inspection machine helps operators see holes, stains, oil marks, slubs, missing yarns, colour variation, bowing, skewing, creases, needle lines, and printing, dyeing or selvage defects. Most machines are operator-assisted, so what gets identified depends on lighting, fabric tension, running speed and the inspector's training and experience.

Start with your fabric: type, width, roll diameter and whether it is woven or knitted. Then compare lighting, speed control, tension handling, length measurement, defect marking and build quality. Check your buyer's inspection requirements, ask the manufacturer about service and calibration support, and consider total cost rather than price alone.

It's used to check fabric rolls for defects like holes, stains and colour differences before cutting. It also measures length and helps teams record and grade fabric quality.

It moves the fabric over a lit surface at a steady speed. An operator watches for flaws, marks them, and the machine measures length while rewinding the roll.

It finds problems early, before the fabric is cut. That helps you avoid wasted material, sort fabric by quality, and share clear records with suppliers and buyers.

Common ones include holes, stains, slubs, missing yarns, shade variation, bowing, skewing, creases, needle lines, and printing or dyeing faults.

```
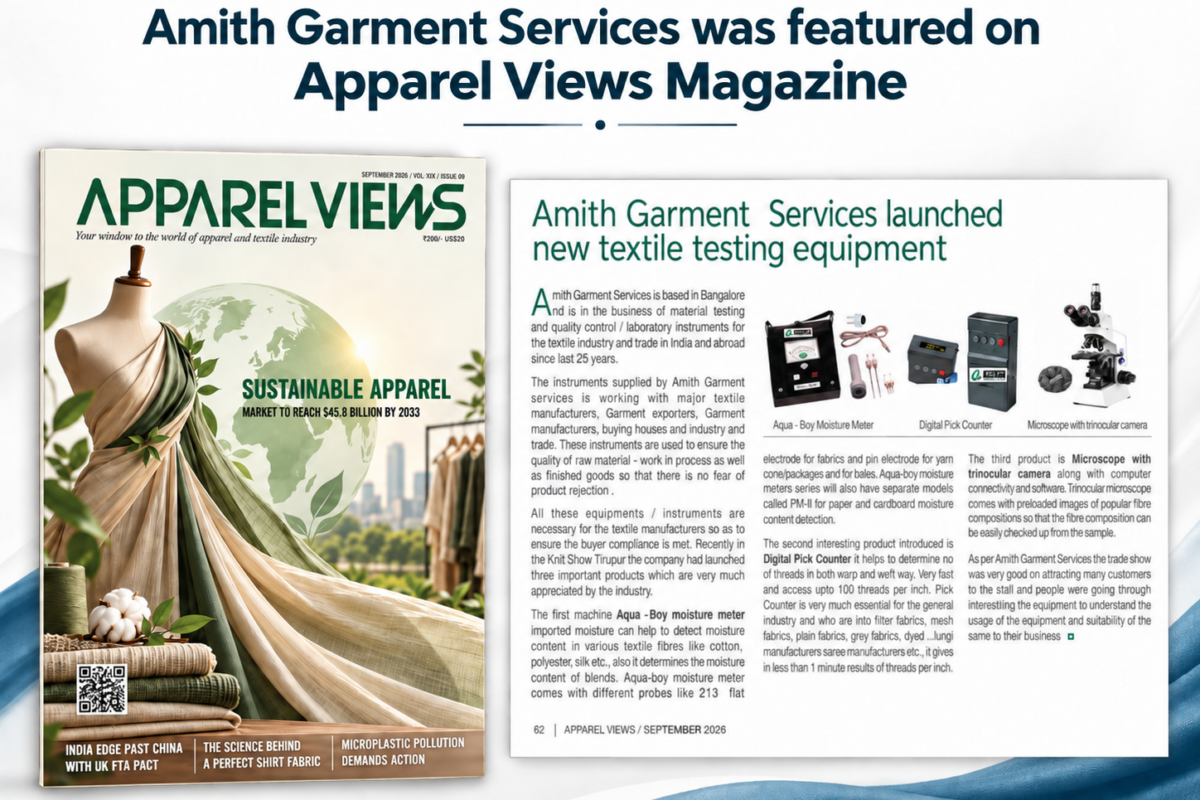
Amith Garment Services featured in Apparel Views Magazine September 2026 for textile testing equipment and quality control solutions.

Amith Garment Services Featured in Apparel Views Magazine for Advanced Textile Testing Equipment

Amith Garment Services is pleased to announce its feature in the September 2026 edition of Apparel Views Magazine, highlighting the company’s contribution to textile testing, quality control, and laboratory instrumentation. The feature, titled “Amith Garment Services launched new textile testing equipment,” appears in the magazine’s September 2026 issue and focuses on the company’s role in supporting textile manufacturers, garment exporters, buying houses, and other industry stakeholders with practical testing solutions.

For more than 25 years, Amith Garment Services has been associated with the material testing and quality-control segment of the textile industry. Based in Bangalore, the company supplies laboratory and textile testing instruments used across different stages of manufacturing, helping businesses evaluate raw materials, work-in-process materials, and finished goods.

Being featured in an industry publication such as Apparel Views is an important milestone for Amith Garment Services. It reflects the growing importance of accurate testing, quality assurance, and measurement technologies in a textile market where manufacturers are expected to maintain consistency, satisfy buyer requirements, and reduce the risk of product rejection.

Supporting Quality Control Across the Textile and Garment Industry

Quality control is a critical part of textile manufacturing. From fibre and yarn to fabric and finished garments, manufacturers need reliable testing methods to understand whether materials meet required specifications.

According to the magazine feature, Amith Garment Services works with textile manufacturers, garment exporters, garment manufacturers, buying houses, and other businesses in the textile trade. The testing instruments supplied by the company are used to help assess quality at different stages of production.

In practical terms, textile testing can support manufacturers in checking characteristics such as moisture content, thread density, fibre composition, and other measurable properties before products proceed to the next stage of manufacturing or dispatch.

This becomes particularly important for export-oriented manufacturers, where quality deviations may result in additional inspection, delays, reprocessing, rejection, or commercial disputes. A systematic approach to testing therefore supports both quality assurance and more consistent manufacturing processes.

New Textile Testing Equipment Highlighted in Apparel Views

The Apparel Views feature highlights three testing solutions introduced by Amith Garment Services and presented to the textile industry:

  1. Aqua-Boy Moisture Meter
  2. Digital Pick Counter
  3. Microscope with Trinocular Camera

The article notes that these products were presented at the Knit Show Tirupur and received interest from industry visitors.

Each instrument serves a different testing requirement and can support manufacturers in improving their understanding of material properties.

Aqua-Boy Moisture Meter for Textile Moisture Measurement

Moisture content can influence the processing, storage, handling, and quality of textile materials. Fibres naturally interact with moisture in the surrounding environment, and different materials can respond differently depending on humidity, storage conditions, and fibre composition.

The Aqua-Boy Moisture Meter highlighted in the magazine is designed to help measure moisture in textile fibres such as cotton, polyester, silk, and blends. The article also describes the availability of different probes for different textile applications.

For textile manufacturers, moisture measurement can be useful during incoming material inspection, production, storage, packaging, and dispatch. Maintaining awareness of moisture levels can help manufacturers identify variations before they affect subsequent operations.

The publication also refers to flat electrodes for fabrics and pin electrodes for yarn cones, packages, and bales, indicating that the system can be configured for different material forms. It further mentions separate Aqua-Boy models designed for paper and cardboard moisture measurement.

This makes moisture testing relevant not only to textile production but also to associated packaging and material-control applications.

Digital Pick Counter for Warp and Weft Measurement

Fabric construction plays an important role in fabric appearance, weight, strength, performance, and consistency. One of the commonly evaluated parameters is the number of threads present within a given area of fabric.

The second product highlighted in the article is the Digital Pick Counter, which is used to determine thread counts in both warp and weft directions. According to the magazine feature, the equipment can measure thread density up to 100 threads per inch and provide results quickly.

This type of measurement can be particularly useful for manufacturers, fabric inspection departments, testing laboratories, and quality-control teams handling different fabric constructions.

The article refers to its potential use with filter fabrics, mesh fabrics, plain fabrics, grey fabrics, dyed fabrics, lungi materials, and saree fabrics.

For textile businesses working with multiple suppliers or fabric specifications, a digital pick counter can help provide objective measurements instead of relying only on visual inspection.

Microscope with Trinocular Camera for Fibre Examination

The third solution featured is a microscope with trinocular camera, designed for closer examination of textile fibres.

According to Apparel Views, the microscope can be connected to a computer and used with software, while preloaded images of common fibre compositions can support the examination of fibre samples.

Microscopic examination can be valuable in textile testing because many fibre characteristics cannot be reliably evaluated with the naked eye. Magnified observation may help laboratories and quality-control teams study fibre structures and compare samples when investigating composition or material differences.

The addition of a trinocular camera also makes it easier to view observations on a computer screen, document samples, and potentially maintain visual records as part of laboratory or quality-control processes.

For educational institutions, textile laboratories, manufacturing facilities, buying houses, and inspection teams, such equipment can provide a more practical way to examine fibres and support material evaluation.

Why Textile Testing Matters More Than Ever

The textile and apparel industry is becoming increasingly quality conscious. Buyers today expect consistency not only in appearance but also in measurable characteristics such as fabric construction, material composition, moisture behaviour, dimensional properties, strength, and finishing performance.

Testing helps manufacturers move from assumptions to measurable data.

A reliable testing process can support several important objectives:

  • checking raw materials before production;
  • identifying variations during manufacturing;
  • verifying fabric or yarn characteristics;
  • supporting buyer specifications;
  • reducing avoidable quality disputes;
  • improving consistency between production batches;
  • supporting documentation and internal quality systems.

Testing should not be viewed only as a final inspection activity. When integrated throughout production, it can serve as an early-warning system that allows manufacturers to identify issues before they become costly.

Helping Manufacturers Reduce Quality Risks

Product rejection can create financial and operational challenges for manufacturers. A rejected fabric lot or garment order may lead to rework, replacement costs, production delays, additional freight, and customer dissatisfaction.

The Apparel Views article specifically notes that instruments supplied by Amith Garment Services are used to support quality evaluation of raw materials, work-in-process materials, and finished goods with the objective of reducing the possibility of product rejection.

This reflects an important principle in modern quality management: problems are easier to manage when detected early.

For example, if fabric construction does not match a required specification, identifying the issue before cutting and stitching may prevent further value from being added to a non-conforming material. Similarly, monitoring moisture levels during storage or production may help identify conditions that require attention before material progresses further.

Testing equipment therefore contributes not only to inspection but also to better process control.

Serving Textile Manufacturers, Exporters and Buying Houses

Amith Garment Services operates within a broad textile ecosystem.

The company’s solutions are relevant to:

Textile manufacturers, who may require testing during fibre, yarn, fabric, dyeing, finishing, or production stages.

Garment manufacturers, who need to evaluate incoming fabrics and maintain quality standards before garment production.

Garment exporters, who must meet customer specifications and maintain consistency across export orders.

Buying houses, which often coordinate between buyers and manufacturing facilities and may require independent or internal quality checks.

Testing and quality-control laboratories, where reliable instrumentation is central to day-to-day operations.

Educational and research institutions, which may use textile testing equipment for teaching, demonstration, material analysis, and research.

This broad applicability explains why testing technologies continue to remain important across different parts of the textile value chain.

Industry Engagement at Knit Show Tirupur

The magazine feature also refers to Amith Garment Services presenting its new equipment at the Knit Show Tirupur. The publication reports that visitors showed interest in understanding the equipment, its operation, and its suitability for their businesses.

Trade exhibitions provide an important opportunity for manufacturers to interact directly with testing-equipment suppliers. Unlike product brochures or online descriptions, exhibitions allow users to see instruments, understand how measurements are taken, discuss specific applications, and determine whether equipment suits their production requirements.

For a company operating in a technical field such as textile testing, these face-to-face demonstrations can be particularly valuable.

A Milestone for Amith Garment Services

The September 2026 feature in Apparel Views Magazine represents an important recognition for Amith Garment Services and its continued involvement in India’s textile testing and quality-control sector.

The magazine itself identifies the issue as September 2026, Volume XXV, Issue 09, reinforcing the feature’s place within an established textile and apparel industry publication.

For Amith Garment Services, the feature is not simply about introducing three instruments. It also highlights a larger commitment to helping textile businesses make informed quality decisions through practical measurement and testing technologies.

As textile manufacturing continues to evolve, manufacturers will increasingly depend on accurate information about the materials they process. Moisture measurement, fabric construction analysis, fibre examination, and other forms of laboratory testing can play an important part in maintaining consistency and improving quality assurance.

Moving Forward with Reliable Textile Testing Solutions

With more than 25 years of involvement in material testing and quality-control instruments, Amith Garment Services continues to support textile businesses in Bangalore and beyond with solutions for manufacturing and laboratory requirements.

The company’s feature in Apparel Views Magazine reflects both its industry presence and the increasing relevance of textile testing technologies in modern manufacturing.

From the Aqua-Boy Moisture Meter for moisture measurement to the Digital Pick Counter for warp and weft analysis and the Microscope with Trinocular Camera for fibre examination, the equipment highlighted in the article addresses practical testing needs across the textile value chain.

For textile manufacturers, exporters, buying houses, laboratories, and quality-control professionals, having the right testing equipment can contribute to better measurement, more consistent processes, informed decision-making, and stronger quality assurance.

Amith Garment Services remains committed to supporting the textile and garment industry with testing and quality-control solutions designed for real-world manufacturing requirements.


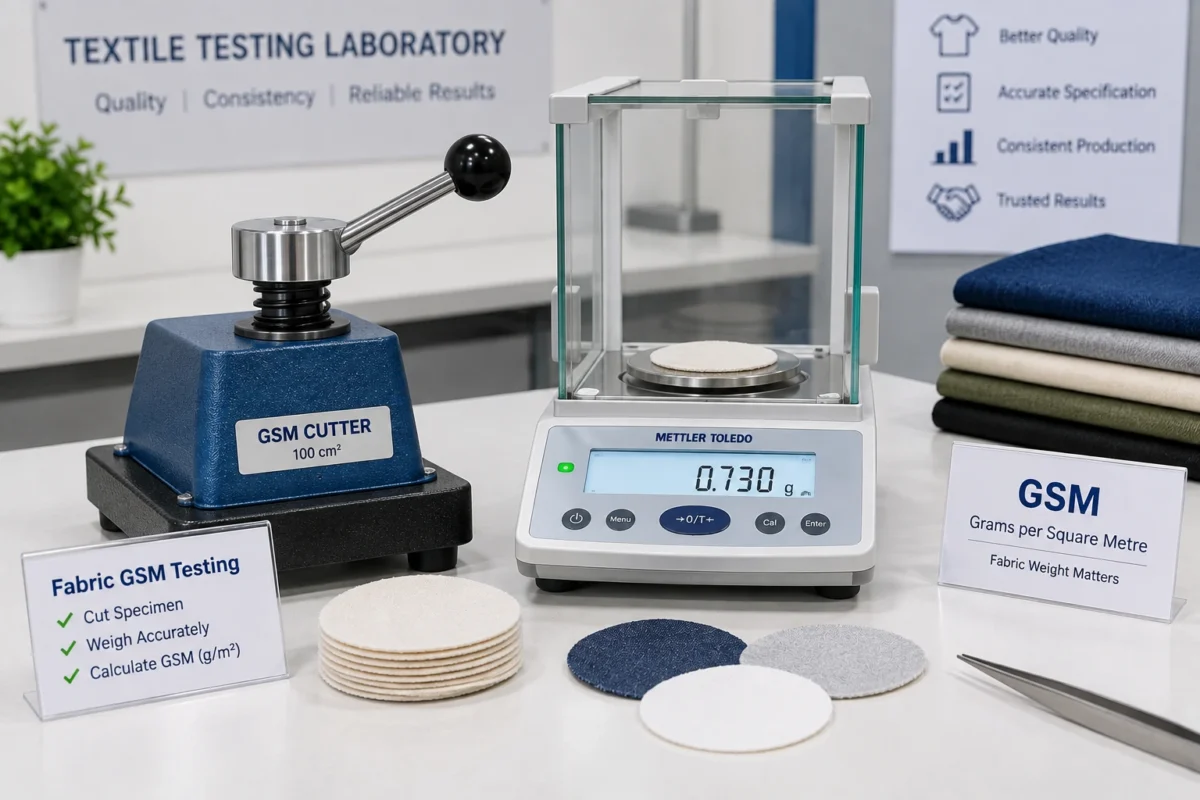
GSM Machine for fabric weight testing in textile laboratory

What Is a GSM Machine and How Does It Work?

If you have spent any time in a fabric mill, a garment factory, or a buying house quality lab, you have probably heard someone ask, “What’s the GSM on this fabric?” It’s one of the first questions raised when a new fabric lot arrives, and for good reason. Fabric weight tells you a lot about how a material will behave — how it drapes, how it feels, how much yarn goes into it, and whether it meets the specification a buyer signed off on.

This is where a GSM Machine comes in. It’s a simple but essential piece of textile testing equipment used to determine how many grams a square metre of fabric weighs. Whether you’re running a spinning mill, managing quality at a garment export unit, or studying textile engineering, understanding how this instrument works will help you read fabric specification sheets with more confidence and catch quality issues before they become costly.

In this article, we’ll walk through what GSM actually means, how a GSM testing machine works step by step, and why this small but important test plays such a big role in textile manufacturing and garment exports.

What Is a GSM Machine?

GSM stands for Grams per Square Metre — a standard unit used across the textile industry to express fabric weight. A GSM Machine, sometimes called a GSM tester or fabric weight tester, is a laboratory instrument used to measure this value on a fabric sample.

In simple terms, fabric weight is the raw physical weight of a piece of cloth, while GSM is that weight expressed per unit area. Two fabrics can look similar but have very different GSM values depending on yarn thickness, weave density, or knitting structure. That’s why relying on “how heavy it feels” isn’t enough — a proper GSM test gives you a measurable, comparable number.

GSM matters because it directly affects cost, performance, and buyer acceptance. A shirt fabric specified at 120 GSM will behave very differently from one at 200 GSM, even if both are cotton. Getting this number right helps mills, exporters, and quality teams stay aligned on what’s actually being produced.

What is a GSM Machine? A GSM Machine is a textile testing instrument used to measure fabric weight in grams per square metre. It typically works with a precision cutter and a weighing balance to calculate how much a specific fabric area weighs, helping determine fabric quality and consistency.

How Does a GSM Machine Work?

The working principle behind a GSM testing machine is straightforward, even though the process requires care and consistency. Here’s how it typically works in a textile lab:

  1. Fabric sample selection – A representative piece of fabric is chosen, avoiding folds, selvedges, or visibly damaged areas.
  2. Conditioning where required – Depending on the applicable testing procedure, samples may be conditioned at standard temperature and humidity before testing.
  3. Cutting the test specimen – A GSM cutter is used to cut a fabric circle or square of a known, fixed area.
  4. Using a standard specimen size – Round cutters of a defined diameter are common in many labs, since they simplify area calculation.
  5. Weighing the sample – The cut specimen is placed on a precision weighing balance to record its weight in grams.
  6. Calculating fabric GSM – The weight is converted mathematically to represent one full square metre.
  7. Recording and interpreting the result – The final GSM value is logged and compared against the buyer’s specification or internal quality standard.

A simplified GSM calculation example: if a fabric specimen cut to a known area weighs a certain number of grams, that weight is scaled up proportionally to represent a full square metre. For instance, a small circular sample represents a known fraction of a square metre, so the recorded weight is multiplied accordingly to arrive at the final GSM figure. Many GSM testing machines and cutters are designed around standard specimen sizes specifically to make this calculation simple and repeatable.

How does a GSM Machine work? A GSM Machine works by cutting a fabric sample of known area using a GSM cutter, weighing it on a precision balance, and mathematically converting that weight into grams per square metre. This gives a standardized, comparable fabric weight value.

GSM Machine and GSM Cutter – What Is the Difference?

People often use “GSM Machine,” “GSM Tester,” and “GSM Cutter” interchangeably, but each refers to a slightly different part of the testing process.

Component Function
GSM Machine / GSM Tester General term for the overall testing setup used to determine fabric GSM
GSM Cutter Precision tool used to cut a fabric specimen of a fixed, known area
Weighing Balance Precise scale used to record the weight of the cut specimen in grams

In practice, GSM testing usually involves a cutting tool paired with an accurate weighing instrument. Some labs use a combined setup, while others use a dedicated GSM cutter alongside a separate analytical balance. Both components need to work together reliably — an inaccurate cutter or an uncalibrated balance can lead to misleading GSM results, regardless of how good the rest of the process is.

Why Is GSM Testing Important in Textile Manufacturing?

GSM testing isn’t just a lab formality — it has real, practical consequences across the production chain.

  • Maintaining fabric specifications as agreed with buyers or brands
  • Batch-to-batch consistency, especially across large production runs
  • Cost estimation and material consumption planning, since GSM affects how much fabric is needed per garment
  • Production planning, particularly for cutting and sewing operations
  • Garment construction quality, since fabric weight influences drape, structure, and finish
  • Export quality requirements, where buyers often specify acceptable GSM tolerance
  • Detecting variation between different rolls or lots of the same fabric order

Incorrect GSM can affect how a garment hangs, how it feels to the wearer, its durability, and even how it performs in downstream processes like cutting and stitching. A fabric that’s lighter than specified might feel flimsy or transparent, while one that’s heavier than ordered could throw off costing and shipping weight calculations.

Why is GSM testing important? GSM testing is important because it verifies whether fabric meets the specified weight, ensuring consistency across production batches, accurate costing, and compliance with buyer requirements. Incorrect GSM can affect fabric drape, durability, garment appearance, and overall production quality.

GSM Testing Procedure for Fabric

While exact steps can vary depending on the applicable standard or buyer specification, a typical GSM testing procedure in a textile laboratory follows this general workflow:

  • Select a representative area of the fabric roll
  • Avoid creases, stains, torn edges, or visibly defective sections
  • Cut the specimen using a GSM cutter at the chosen location
  • Weigh the specimen accurately on a calibrated balance
  • Record the result along with sample details
  • Repeat the test at multiple points across the fabric where required
  • Calculate the average GSM from multiple readings

Representative sampling matters because fabric weight can vary slightly across a roll due to tension, finishing, or manufacturing inconsistencies. A single reading from one spot doesn’t always reflect the true average GSM of the entire batch, which is why many labs test multiple points rather than relying on just one specimen. It’s worth noting that not every laboratory or buyer follows an identical procedure — the applicable standard or in-house testing protocol should always guide the exact steps taken.

GSM Machine vs Manual GSM Testing

Feature GSM Machine/Tester Manual GSM Testing
Testing process Standardized cutting and weighing setup Estimated or improvised measurement
Accuracy Generally higher, based on calibrated instruments Depends heavily on operator skill and tools used
Speed Faster, especially with dedicated cutters Slower and more labor-intensive
Operator involvement Moderate, with defined steps High, with more room for inconsistency
Repeatability Good, when equipment is calibrated Variable between operators
Laboratory suitability Suitable for regular quality control testing Suitable only for rough, non-critical checks
Quality control use Widely used in structured QC programs Rarely sufficient for buyer compliance

The right setup ultimately depends on your laboratory’s testing volume, accuracy requirements, and the standards you need to comply with. A high-volume export unit will likely need dedicated GSM testing equipment, while a smaller operation might start with basic tools and scale up over time.

Types of Fabrics Tested Using a GSM Machine

GSM testing applies across a wide range of fabric types, including:

  • Cotton fabrics
  • Polyester and synthetic fabrics
  • Blended fabrics (cotton-poly, viscose blends, etc.)
  • Knitted fabrics
  • Woven fabrics
  • Nonwoven materials, where applicable
  • Garment-specific fabrics
  • Home textile materials like bedsheets and curtains

GSM ranges vary significantly depending on fabric construction, fiber type, and intended end use. A lightweight shirting fabric will naturally sit at a very different GSM than a heavy denim or upholstery fabric, so there’s no single “ideal” number — it’s always relative to what the fabric is designed for.

Factors That Can Affect Fabric GSM

Several variables can influence the final GSM reading, including:

  • Fibre composition and yarn count
  • Fabric construction (knit vs woven)
  • Ends and picks per inch in woven fabrics
  • Knitting structure and stitch density
  • Finishing processes like calendering or coating
  • Moisture content in the fabric
  • Fabric shrinkage after washing or processing
  • Location on the fabric roll where the sample was taken
  • Conditioning of the sample before testing
  • Overall measurement accuracy of the equipment used

Because so many factors can shift the result, testing conditions and sampling consistency matter just as much as the equipment itself. A well-calibrated GSM machine used with poor sampling practices will still produce unreliable results.

GSM Machine in Textile Quality Control

GSM testing plays a role at multiple checkpoints in the quality control process:

  • Incoming fabric inspection from suppliers
  • In-process quality checks during production
  • Final fabric inspection before cutting
  • Buyer compliance verification
  • Supplier performance evaluation
  • Batch-to-batch comparison
  • Ongoing production monitoring
  • Garment quality testing before shipment

Rather than relying on a single GSM reading, experienced quality teams track variation across multiple samples and batches over time. This helps identify whether a supplier is consistently within tolerance or whether a particular lot needs closer inspection.

How is GSM used in textile quality control? In textile quality control, GSM testing helps verify incoming fabric against specifications, monitor consistency across production batches, and confirm buyer compliance. Quality teams often track GSM trends across multiple samples rather than depending on a single test result.

How to Choose the Right GSM Machine

Selecting suitable GSM testing equipment depends on several practical factors:

  • Required measurement accuracy for your testing needs
  • Testing range suitable for your fabric types
  • Sample size requirements based on your standard procedure
  • Ease of operation for lab staff
  • Build quality and durability of the cutter and balance
  • Laboratory environment and available space
  • Calibration requirements and frequency
  • Repeatability of results over repeated use
  • Compatibility with your applicable testing standard
  • Availability of technical support and replacement parts
  • Expected testing volume in your facility

Rather than choosing based on price alone, it’s worth evaluating equipment against your actual testing requirements and the standards your buyers expect you to follow.

GSM Testing Standards and Laboratory Practices

GSM testing is typically carried out based on applicable international, national, or buyer-specific procedures. Different laboratories and buyers may reference different standards depending on the region, product category, or contractual requirement. Rather than assuming one procedure applies universally, it’s good laboratory practice to confirm which standard or buyer specification applies to a given order and to follow its current official version.

If your lab works with multiple buyers, it’s common to maintain records of which testing procedure was used for each order, since requirements can differ from one buyer to another.

Industries That Use GSM Testing

GSM testing is used widely across:

  • Textile manufacturing units
  • Garment manufacturing and export houses
  • Buying houses and sourcing agents
  • Fabric processing and finishing units
  • Independent textile testing laboratories
  • Home textile producers
  • Technical textile manufacturers
  • Quality inspection agencies

India has a strong and diverse textile manufacturing base, with clusters like Tiruppur known for knitwear and garment exports, and cities like Bangalore hosting a mix of textile manufacturers, buying houses, and testing laboratories. Across the broader textile industry — both in India and internationally — GSM testing remains one of the most routinely performed quality checks in fabric and garment production.

Common GSM Testing Mistakes

Even experienced labs can run into avoidable errors, such as:

  • Taking a sample that isn’t representative of the fabric roll
  • Cutting the specimen inaccurately or off-center
  • Using a weighing balance that isn’t properly calibrated
  • Skipping moisture or conditioning requirements when applicable
  • Not checking equipment condition before testing
  • Relying on only one reading instead of an average
  • Poor sample labeling and identification
  • Mixing different testing procedures within the same batch
  • Failing to maintain proper testing records

Consistent laboratory practices — calibrated equipment, trained staff, and clear documentation — go a long way toward improving the reliability of GSM results over time.

Why Choose Amith Garment Services

At Amith Garment Services, we supply GSM Machines, GSM Cutters, and a wider range of textile testing equipment designed to support fabric and garment quality workflows. Our product range includes GSM testing tools, Color Matching Cabinets, Crock Meters, Washing Fastness Testers, Fabric Inspection Machines, Bursting Strength Testers, and Fabric Rolling Machines, among other garment testing instruments.

We work with textile manufacturers, garment exporters, and testing laboratories to help them identify equipment suited to their specific testing requirements, lab environment, and applicable standards. Rather than pushing a one-size-fits-all solution, our approach is to understand what you’re testing, how often, and to what specification — and help you choose accordingly.

If you’re setting up a new fabric testing lab or upgrading existing GSM testing equipment, our team can walk you through the practical considerations involved.

Frequently Asked Questions

A GSM Machine is used to measure the weight of a fabric sample per square metre, helping textile manufacturers and quality teams verify whether fabric matches the required specification. It's commonly used during incoming fabric inspection, in-process quality checks, and final inspection before garments are cut and sewn. By providing a standardized, comparable weight value, a GSM Machine helps reduce guesswork and supports consistent decision-making across fabric batches, suppliers, and production orders.

A GSM Machine typically works by cutting a fabric specimen of a fixed, known area using a GSM cutter, then weighing that specimen on a precision balance. The recorded weight is then mathematically scaled up to represent a full square metre of fabric. This process gives a standardized GSM value that can be compared against buyer specifications or internal quality benchmarks, regardless of the actual size of the fabric roll being tested.

A GSM Cutter is a precision tool used specifically to cut a fabric specimen of a known, fixed area, while a GSM Machine or GSM Tester refers more broadly to the overall testing setup, which includes both the cutting tool and a weighing balance. In practice, both components work together — the cutter ensures a consistent sample size, and the balance provides an accurate weight reading needed to calculate the final GSM value.

Textile manufacturers test fabric GSM to confirm that production output matches agreed specifications, maintain consistency across batches, and avoid costly quality disputes with buyers. GSM directly influences fabric drape, durability, and garment appearance, so even small deviations can affect how a finished product performs. Regular GSM testing also supports better cost estimation, material planning, and long-term supplier evaluation within a textile quality control program.

A GSM Machine is used to measure fabric weight per square metre, helping textile labs check whether fabric meets buyer specifications and stays consistent across production batches.

You test fabric GSM by cutting a sample of known area, weighing it on a precise scale, and calculating the equivalent weight for one full square metre.

Fabric GSM matters because it affects cost, drape, durability, and how a garment feels and performs, making it a key quality check in textile production.

Choose a GSM testing machine based on your accuracy needs, testing volume, applicable standards, and how easily it fits into your existing lab workflow and calibration routine.

color matching cabinet

What Is a Color Matching Cabinet and How Does It Work?

Anyone who has compared a fabric swatch near a window in the morning and then again under office tube lights knows the shade never looks quite the same twice. That shift isn’t imagination — it’s a real optical phenomenon, and it’s one of the biggest headaches in textile production. A color matching cabinet solves this by giving quality teams one fixed, repeatable lighting setup so a colour decision made today matches the decision made next week, whether it’s checked in Bengaluru, Dhaka, or a buyer’s office in Europe.

Colour looks different under different light because light sources emit different wavelengths. A dye recipe that appears identical to a buyer’s standard under daylight can look slightly greenish under fluorescent light and slightly reddish under incandescent light. This effect, known as metamerism, is one of the most common causes of rejected fabric lots, reprocessing costs, and disputes between mills and buying houses. Since no factory or lab can control the weather or the time of day, textile manufacturers rely on artificial, standardized lighting instead — and that’s exactly what this equipment provides.

What Is a Color Matching Cabinet?

A color matching cabinet is a controlled-lighting viewing booth used in textile and garment quality control to evaluate and compare fabric colour under standardized artificial light sources instead of variable daylight or room lighting. It houses multiple lamp types — such as daylight, TL84, and UV — so that inspectors can view a sample under the exact same conditions every time, anywhere in the world.

Put simply, it’s a shading cabinet: an enclosed, neutral-grey interior lined with specific light sources, built so that stray light, wall colour, and ambient reflections don’t interfere with the assessment. Fabric swatches, lab dips, garment panels, and approved standards are placed side by side inside, and the inspector switches between light sources to check whether the shade holds up consistently. This is why the equipment is also referred to as a color matching box, color matching light box, or simply a textile color matching cabinet — the terms are used interchangeably across mills and labs.

Viewing fabric under uncontrolled room lighting is unreliable because ordinary tube lights, LED panels, and daylight through a window all have different colour temperatures and spectral compositions. A shade that passes inspection under one type of light might fail under another, which is exactly the kind of inconsistency a fabric color matching cabinet is designed to eliminate.

Why Is a Color Matching Cabinet Important in Textile Testing?

Colour is often the first thing a buyer notices, and it’s also one of the most common reasons for rejection at the inspection stage. A color assessment cabinet matters in textile testing because it removes guesswork from decisions that directly affect production cost and buyer relationships. Here’s where it plays a role:

  • Fabric colour approval – Lab dips and bulk production samples are checked against an approved standard before dyeing continues at scale.
  • Shade matching – Panels cut from different rolls or dye lots are compared to confirm they fall within an acceptable tolerance.
  • Production consistency – Repeated checks across shifts and batches use the same lighting, so results aren’t influenced by the time of day.
  • Buyer approvals – Many international buyers specify the exact light source (often D65) their vendors must use, and a textile color matching cabinet ensures the factory can meet that requirement precisely.
  • Garment quality testing – Finished garment panels, trims, and accessories are checked together to confirm they match as a set.
  • Dyeing quality control – Dye house teams use it to catch shade variation early, before an entire lot is processed incorrectly.
  • Fabric color assessment across suppliers – When fabric arrives from multiple vendors, the cabinet gives a common reference point for comparison.
  • Textile color inspection at multiple production stages – from greige to finished fabric to cut panels.

Without this kind of controlled environment, two equally experienced inspectors could reach different conclusions about the same fabric simply because one checked it near a window and the other under a ceiling light.

Color Matching Cabinet Working Principle

The color matching cabinet working principle is straightforward once you understand what it’s trying to solve. The cabinet houses several individually switchable light sources, each simulating a specific real-world lighting condition:

  • D65 – Simulates average daylight; the most commonly specified reference for international buyers.
  • TL84 – Simulates fluorescent lighting typically found in European retail stores.
  • CWF (Cool White Fluorescent) – Common in North American retail environments.
  • UV (Ultraviolet) – Detects optical brighteners or whitening agents used in fabric finishing.
  • Incandescent (A) – Simulates warm household lighting.
  • Horizon light / TL83 in some models, for additional retail simulation.

The interior walls are typically finished in a neutral grey to avoid any colour bias reflecting onto the sample. The inspector places the fabric or garment sample alongside the approved standard, closes the cabinet to block external light, and switches between light sources one at a time. If the shade matches consistently across all the specified lights, it’s considered a stable match. If the colour shifts noticeably under one or more sources, that’s metamerism showing up — and it flags a real risk that the same fabric could look mismatched once it reaches the buyer’s store under different lighting.

This is the basic operating logic behind every textile color matching machine on the market, regardless of brand or cabinet size, and it’s the same principle taught in most textile quality control training programs.

Standard Light Sources Used for Color Matching

Every reputable standard light source for color matching used in these cabinets follows internationally recognized illuminant standards, largely based on CIE (International Commission on Illumination) definitions. Buyers and certification bodies usually specify which combination of lights a supplier must check against — commonly D65 plus TL84, with UV used separately to detect brightening agents. Using the correct, calibrated light source matters just as much as using the cabinet itself; a poorly calibrated or aging lamp can quietly throw off every assessment made under it, which is why periodic lamp replacement and calibration checks are part of standard lab maintenance.

Where Color Matching Cabinets Are Used in the Textile Industry

The use of a color matching cabinet in textile industry settings spans the entire supply chain:

  • Textile mills and dye houses – checking lab dips against approved standards before bulk dyeing
  • Garment manufacturing units – matching fabric, thread, buttons, zippers, and trims as a complete set
  • Buying houses and merchandising offices – verifying supplier samples before forwarding approval to the buyer
  • Textile testing laboratories – running formal colour fastness and shade comparison tests
  • Quality control departments – conducting routine inline and end-line inspections
  • Export houses – confirming shipment-ready goods meet the buyer’s specified colour tolerance

This wide range of use is one reason visual color matching remains a standard practice even in facilities that also use spectrophotometers for numerical colour measurement — the human eye, under correct lighting, is still the final check before goods are approved.

Visual Color Matching vs. Instrumental Color Measurement

It’s worth noting that a color matching cabinet supports visual assessment, while a spectrophotometer provides numerical, instrument-based colour data (values like L*, a*, b*, and Delta E). The two methods complement each other rather than replace one another. Instrumental measurement is useful for objective, repeatable data, but many buyers still require final sign-off through visual inspection under standardized light, since that reflects how the product will actually be judged by end customers in a retail setting. A well-run quality department typically uses both: instrumental data to catch deviations early, and the cabinet for final human approval.

Choosing the Right Color Matching Equipment

When selecting color matching equipment for a lab or production floor, a few practical factors matter more than brand names:

  • Number and type of light sources included, matched to your buyers’ requirements
  • Cabinet size, based on whether you’re checking swatches, full garment panels, or large fabric rolls
  • Build quality of the interior lining, since colour-neutral walls are essential for accurate results
  • Lamp availability for replacement, since consistent recalibration keeps results reliable over time
  • Ease of switching between light sources during inspection

Getting this right the first time avoids the common problem of a factory investing in a cabinet that doesn’t match the light sources its buyers actually specify.

Conclusion

A color matching cabinet isn’t a luxury item in a textile lab — it’s the equipment that keeps colour decisions consistent across shifts, teams, and continents. By replacing unpredictable daylight and mixed room lighting with standardized artificial sources, it takes the guesswork out of shade approval and helps catch metamerism before it becomes an expensive rejection at the buyer’s end. Whether it’s called a color matching box, a color matching light cabinet, or a fabric color matching cabinet, its job stays the same: give inspectors one reliable, repeatable way to judge colour, every single time.

Frequently Asked Questions

A color matching cabinet is used to evaluate and compare fabric or garment colour under standardized artificial light sources, helping textile professionals confirm shade accuracy before production or shipment approval.

D65, which simulates average daylight, is the most widely specified standard light source for color matching, often used alongside TL84 and UV depending on the buyer's requirements.

This happens due to metamerism, where two colours that appear to match under one light source look different under another because of differences in their spectral reflectance.

No. A color matching cabinet supports visual color matching under controlled lighting, while a spectrophotometer measures colour numerically. Many textile labs use both together for complete quality control.

Lamps degrade with use and should be checked and replaced periodically, typically as recommended by the manufacturer, since an aging lamp can distort colour assessment results even if it still lights up normally.

It ensures fabric color assessment, textile color inspection, and shade approvals are done consistently, reducing disputes between mills, garment manufacturers, and buyers over colour mismatches.